The Job Is Released. Why Is Production Still Waiting for Material?
Released work is not production-ready when critical material is late, unallocated, in the wrong location or consumed by competing demand. Epicor should help management distinguish released jobs from truly executable jobs.
The short answer
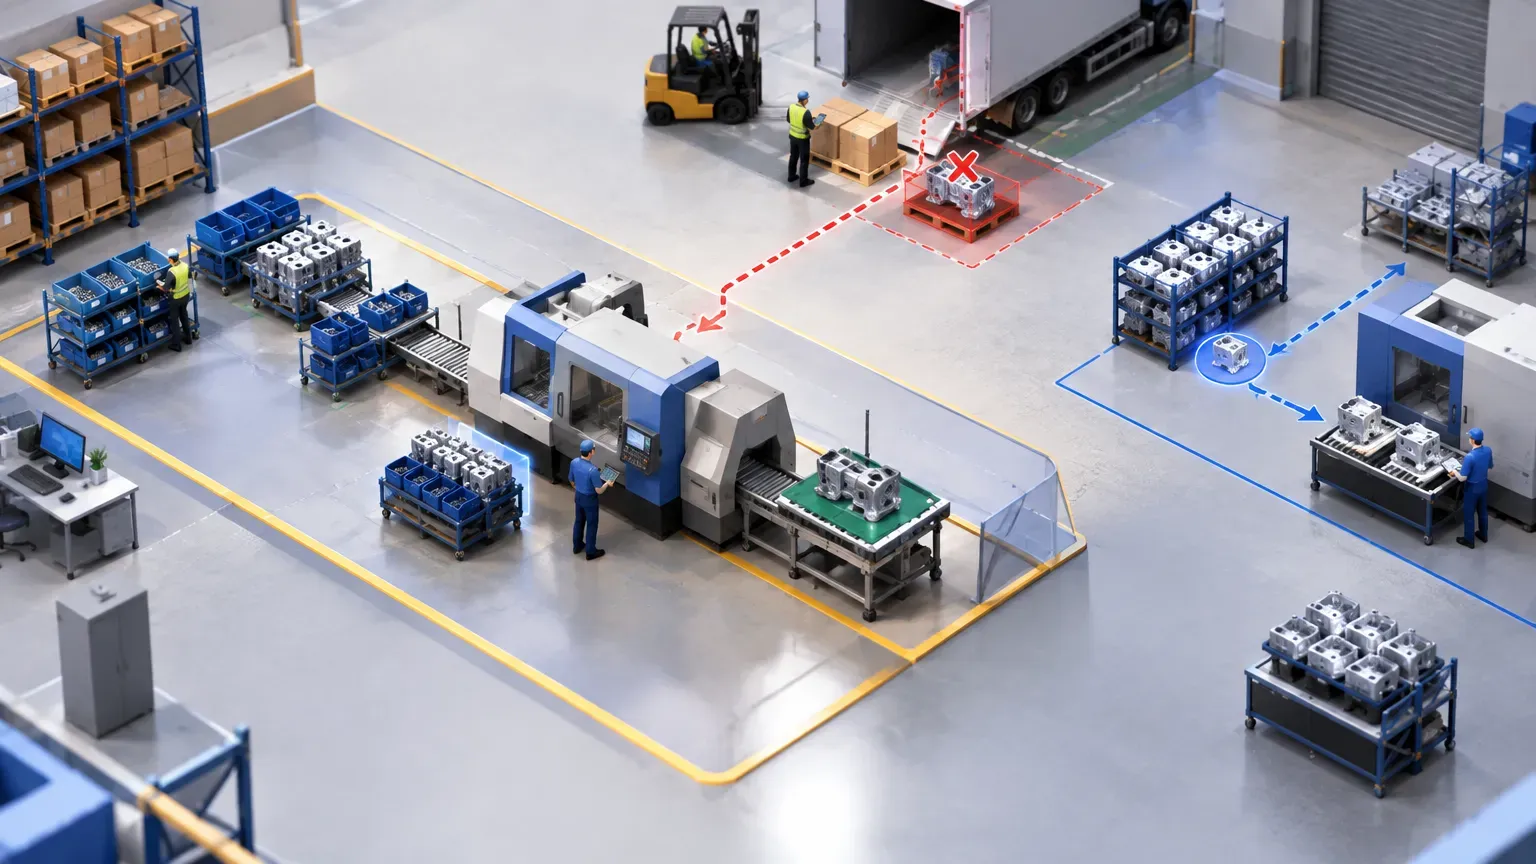
A released job is not truly production-ready until the material needed for the next meaningful work is available, usable and in the right operational place. Epicor users should distinguish released demand from executable demand so supervisors do not discover shortages only after labour and capacity have already been committed.
Material readiness is therefore a production-control question, not only an inventory or purchasing question.
How this connects to the pillar
The broader plan-to-profit model is covered in Epicor Has the Orders. Can Management See Which Ones Will Actually Make Money?. Material readiness determines whether the planned job can actually convert capacity into output.
On-hand does not mean ready
A component can appear on hand and still be unusable for the job.
It may be:
- allocated to another order;
- in a different warehouse;
- under quality hold;
- waiting for inspection;
- in a staging location;
- reserved for service;
- physically missing despite system balance;
- available in the wrong unit or configuration.
Readiness needs an operational definition.
Define the material horizon
Not every component needs to be physically present before a job starts.
Some materials are required only at later operations.
The correct readiness horizon depends on the routing and the risk of interruption.
A sensible rule might protect the first several operations or the known critical components rather than insist on complete kit availability for every job.
The important point is to define the rule rather than let every supervisor decide differently.
Identify critical components
Some parts are easy to replace or obtain.
Others can stop the job entirely.
Classify components by their effect on execution.
Long-lead, single-source, custom, regulated or difficult-to-substitute items may need earlier attention than standard consumables.
This helps planning focus on the shortages that genuinely threaten production.
Separate purchased shortage from internal shortage
A component can be missing because the supplier is late.
It can also be missing because an internal transfer was not posted, a prior operation has not completed, material is sitting in inspection or the location record is unreliable.
Do not send every shortage to purchasing.
Trace whether the root cause is supply, inventory execution, production timing or master data.
That keeps the corrective action with the right owner.
Use expected receipts cautiously
An open purchase order may support planning, but it is still an assumption.
Supplier date reliability, transport and inspection can all affect when the material is truly usable.
For high-risk components, compare expected receipt with historical reliability and current evidence.
The aim is not to distrust suppliers. It is to avoid treating a planned date as the same thing as executable material.
Protect scarce material from priority churn
When priorities change frequently, scarce material can be reallocated repeatedly.
One job becomes ready by making another job not ready.
If the business does this consciously, that may be appropriate.
But the effect should be visible.
Material allocation decisions should connect to customer priority and schedule consequences rather than happen informally at the warehouse or shop floor.
Improve staging discipline
Material can be available in Epicor and still consume production time if it is not staged or easy to locate.
For high-volume or constrained processes, define when and where material should be prepared before the job reaches the resource.
Staging status can become part of readiness evidence.
This is especially valuable where setup windows are short and searching for material consumes constrained capacity.
Treat substitutions as controlled exceptions
Substitution can protect delivery.
It can also create quality, cost or traceability consequences.
Where substitutions are allowed, define who can authorize them, what technical rules apply and how the material change reaches Epicor.
Frequent substitution of the same component may indicate sourcing or master-data work is needed.
Connect shortages to profitability
Material shortage is often discussed as a delivery issue.
It can also create cost:
- premium freight;
- higher purchase price;
- overtime;
- idle labour;
- schedule disruption;
- extra setups;
- partial shipments;
- expediting effort.
Linking shortage cause to cost makes supply risk part of the plan-to-profit conversation.
What management should measure
Useful indicators include:
- released jobs not material-ready;
- critical shortages by cause;
- jobs started with known shortages;
- supplier-related versus internal shortages;
- premium freight linked to shortage;
- material reallocation caused by priority changes;
- time lost searching or staging material;
- substitution frequency;
- repeated shortages by component family;
- jobs delayed despite apparent on-hand inventory.
These measures show whether the problem is supply, planning or execution.
ACC context
ACC supports Epicor planning, inventory and manufacturing workflows. Material readiness improves when the ERP view of demand and supply is connected closely to the physical reality of where material is, whether it is usable and which job has the right to consume it. Explore ACC’s Epicor capabilities.
Operational review point
Take five jobs that were released but could not start on time.
For each job, identify the first component that blocked execution.
Then classify the cause: supplier, internal transfer, quality, allocation, location, planning or master data.
The pattern usually identifies a more useful improvement than simply increasing safety stock.
Use shortage age, not only shortage count
A short-lived shortage may resolve before it affects production.
An old shortage on a critical component deserves different attention.
Track how long important shortages remain unresolved and whether the expected resolution date keeps moving.
Age helps separate normal planning noise from persistent supply or process risk.
Link engineering changes to material readiness
A job can lose readiness after an engineering change.
New material may be required, existing stock may become unusable or purchasing may need a different specification.
Change control should therefore reconnect the job to material-readiness review rather than assuming the original supply plan remains valid.
This is especially important for engineered products where late changes are common.
Review excess created by priority changes
Material purchased or staged for a job can become excess when demand moves, the design changes or the schedule is repeatedly reprioritized.
That cost may not appear as a shortage, but it is part of the same planning discipline.
Review whether urgent decisions are creating stranded inventory elsewhere in the plan.
Connect safety stock to shortage cause
Safety stock can protect service when demand or supply is variable.
It is less effective when shortages come from internal posting delay, allocation confusion or wrong-location inventory.
Before increasing buffer, classify the shortage history.
If most shortages arise from genuine supplier variability, inventory policy may help. If they arise from execution, additional stock can increase working capital without fixing readiness.
Make shortage escalation time-based
Critical shortages become more expensive as the planned start approaches.
Define escalation points based on time to need, component criticality and available recovery options.
An unresolved long-lead shortage several weeks out may need supplier action; the same shortage hours before production may require a management decision about resequencing, substitution or customer commitment.
Time-based escalation keeps attention proportional to urgency.
Use readiness to control job release
If the business releases large numbers of jobs long before they can execute, the production queue becomes harder to interpret.
Consider whether release policy should include selected readiness criteria for near-term work.
This does not mean every component must be available.
It means release should communicate a meaningful level of execution intent instead of becoming an administrative milestone disconnected from reality.
Measure readiness failure at the first operation
A useful test is simple: when the job reaches its intended first operation, can the team begin without searching, waiting or escalating?
Record the reason when the answer is no.
This creates direct evidence about the quality of planning, staging and material control.
Review readiness by product family
Some product families repeatedly fail readiness for the same reasons. Grouping the evidence can reveal structural sourcing, staging or engineering dependencies that are hard to see one job at a time.
This makes recurring gaps easier to assign and improve.
Frequently asked questions
Should every job be fully kitted before release?
Not necessarily. Define the appropriate readiness horizon based on routing, component criticality and interruption risk.
Is purchase-order due date enough to treat material as available?
No. It is planning evidence, but actual usability may depend on supplier reliability, transport, inspection and receipt timing.
Who owns material readiness?
It is cross-functional. Planning defines the need, purchasing manages external supply, inventory controls physical availability and operations confirms executable readiness.
Can more inventory solve material-readiness problems?
Sometimes, but not when the root cause is allocation, timing, location accuracy, quality hold or weak execution discipline.