

Every Carton Has a History. Can Your Factory Reconstruct It?
Traceability is not a serial number at dispatch. It is the connected history of specification, substrate, artwork, operations, quantities, quality decisions and delivery.
The short answer
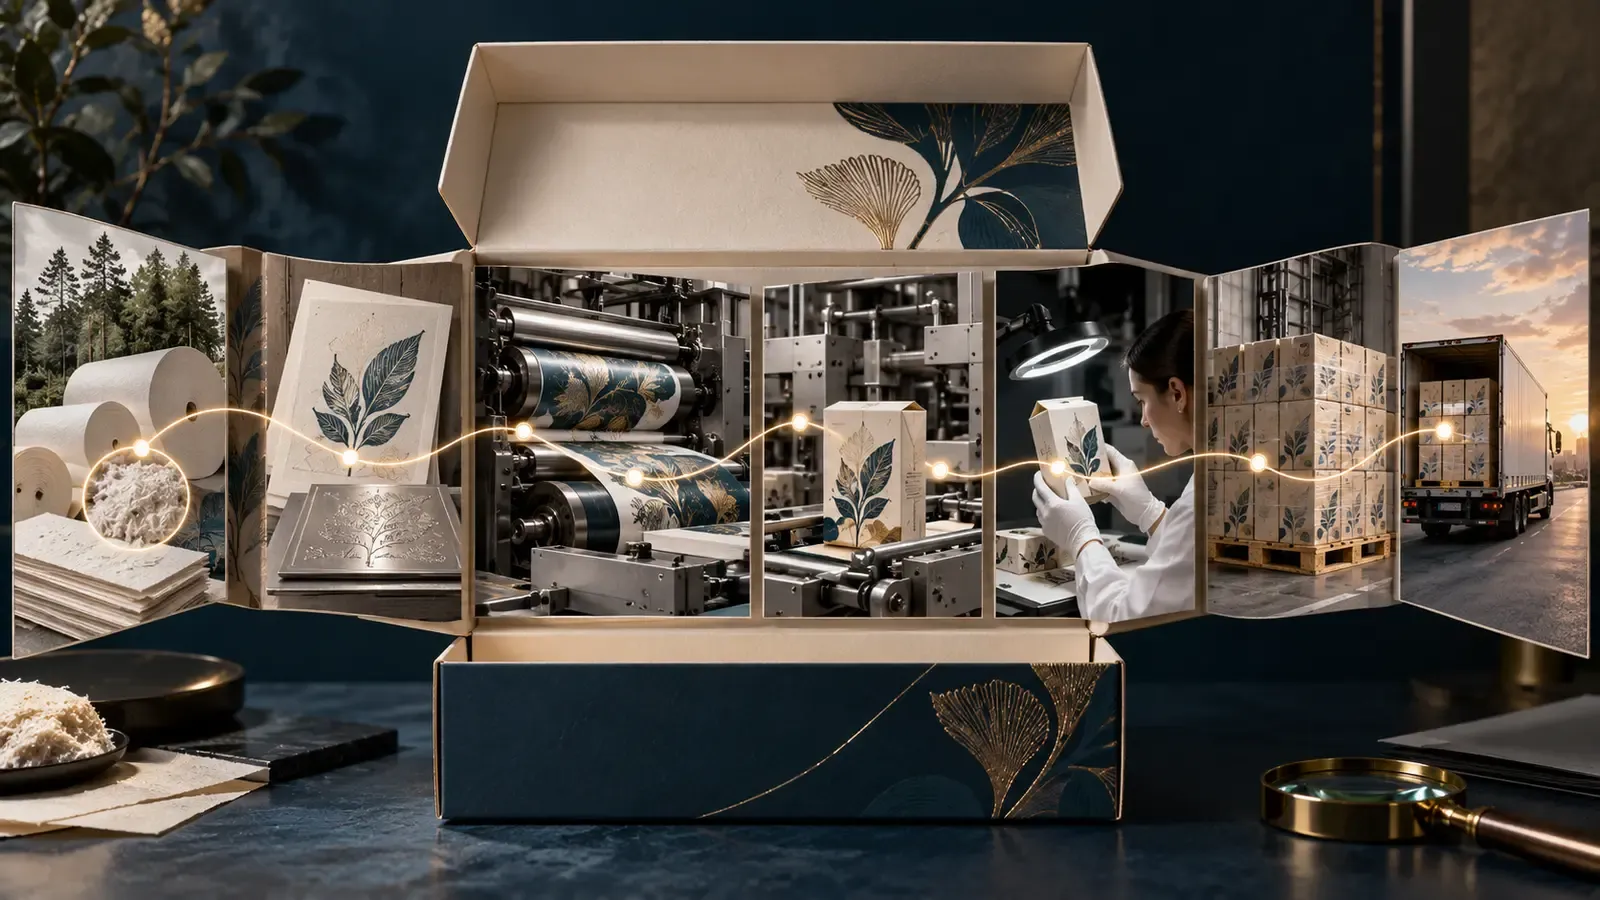
Useful printing and packaging traceability is the ability to reconstruct what happened to a specific customer quantity: which specification and artwork governed it, which substrate lot entered it, which operations transformed it, which quality decisions released it and which shipment carried it. A barcode can help retrieve that history, but the history must first be connected.
One carton on a conference table
A customer places a carton on the table. The colour looks different from the approved sample, and a crease has begun to crack. They ask three simple questions: Was every carton in the delivery made this way? Which material was used? What will you do with the stock already in our warehouse?
Inside the factory, the search begins. Sales finds the order. Prepress finds two artwork files. Purchasing confirms the board grade, but not the lot. Production remembers changing a setting midway through the run. Quality has a retained sample without a batch reference. Dispatch knows which pallets left, but not which production quantities they contained.
Everyone has information. Nobody yet has the history of the carton.
Traceability is a chain of identities
The chain starts with stable identities that survive handoffs:
- customer order and product;
- active specification and artwork revision;
- material item, supplier lot and internal lot;
- job, batch and operation;
- tooling, plate or imposition version where relevant;
- good, rejected, held and reworked quantities;
- inspection and release decision;
- pack, pallet and shipment.
Each identity answers a different question. Together, they allow the factory to move backward from a customer delivery and forward from an affected material lot.
Traceability fails when departments recreate these objects independently. The same substrate may be described by a supplier code, warehouse nickname and estimating description. The same artwork may exist under several filenames. Integration helps only when those identities can be resolved to the same controlled job.
Begin with the decision, not the technology
Before choosing labels, scanners or portals, define what the business must be able to decide.
If a paper lot is found defective, which jobs, batches and shipments could be affected? If a customer reports one carton, can quality identify the likely production batch and retained sample? If a repeat order is released, can prepress prove which revision was used previously and what changed?
These questions determine the necessary granularity. A commodity leaflet may be traced by job batch. Regulated or high-value packaging may require finer control. More detail is not automatically better if people cannot record it reliably.
Follow the material into the job
Commercial material descriptions are not sufficient when physical variation matters. Record supplier lot, received quantity, inspection state, storage location, reservation and issue to the job.
The Paper Was Right. The Lot Was Wrong. examines why two lots with the same specification can behave differently. The traceability model must preserve which lot was consumed by which batch, including substitutions and mixed-lot production.
If unused material returns to stock, retain its identity. If offcuts become usable remnants, define whether their lot and condition remain trustworthy. If several lots feed one run, the resulting output must show the exposure honestly.
Distinguish arrival from readiness
A purchase order marked delivered does not prove that production can use the material. Receiving, inspection, documentation, allocation and conditioning may remain.
The Supplier Met the Date separates physical arrival from production readiness. The distinction matters because a schedule may appear protected while the required roll or board is still held, misplaced or allocated elsewhere.
Material status should therefore express evidence: received quantity, inspection outcome, available quantity, reservation and latest decision time. Procurement, warehouse and planning can then share one operational meaning.
Keep maintenance inside the job history
Machine condition can explain output variation and delivery change. A breakdown, component replacement or adjustment during the batch belongs in the production history.
The Machine Stopped shows how maintenance and scheduling must share a recovery clock. For traceability, record which quantities were produced before and after intervention, what checks were performed and whether any output was held.
This does not mean attaching every maintenance note to every carton. It means preserving events that materially affect the batch, route, quality decision or promise.
Make repeat orders compare, not copy
Repeat business should become easier, but “same as last time” is not a specification.
A Repeat Order Is Never Just the Same Job Again proposes a controlled comparison of artwork, material, quantity, route, tooling and customer instruction. Reuse the accepted baseline while forcing changed elements into view.
This protects both speed and history. The new order can point to the proven predecessor without overwriting it. Later, an investigator can explain which version governed each delivery.
Start complaint investigation from shipment
The customer usually supplies a delivery reference, photograph or sample—not an internal job number. Trace backward from shipment, pallet or product identity to the possible batches and lots.
The Customer Sent One Photo describes how to contain proportionately. The goal is to identify the smallest credible affected population while evidence is gathered.
Weak traceability creates two costly extremes: assume everything is affected, or assume the complaint is isolated without proof. Connected genealogy supports a reasoned boundary.
Turn waste into part of the history
Waste is a quantity outcome of the job, material and operation. It should not disappear into a general bin before its reason and source are captured.
The Waste Bin Is Full of Production Data links waste to setup, defects, trim, overproduction, damage and recovery route. This improves yield, actual cost and sustainability evidence.
Traceability also supports claims about material efficiency. The factory can show what entered, what became saleable product, what was reused and what followed an approved recovery route.
Agree on one management truth
Dashboards often reveal disagreement rather than resolve it. Sales, planning, production, quality and finance may each count a job differently.
One Dashboard, Five Versions of Factory Truth explains why definitions must come before visualisation. A milestone should mean the same event across reports. Quantities must share units and states. Delay needs an agreed reference point.
Traceability is the foundation because every KPI should be explainable back to operational evidence rather than a manually adjusted total.
Design forward and backward tests
Run two practical exercises.
For the backward test, select a shipped pallet and identify the order, product, artwork, production batches, material lots, operations, inspections and release decisions.
For the forward test, select one received material lot and identify remaining stock, jobs that consumed it, output batches, current locations and customer shipments.
Time the exercises and record every break in the chain. Do not help the test by asking the one employee who remembers the job. A resilient system should allow another authorised person to reconstruct it.
Record evidence at natural handoffs
Traceability becomes sustainable when capture aligns with work. Receiving identifies material. Warehouse confirms movement and issue. Prepress releases an artwork version. Production reports batch and quantity. Quality records disposition. Dispatch confirms allocation and shipment.
Avoid asking one department to rebuild everyone’s history at the end. Late entry creates gaps and encourages convenient assumptions.
Scanning can reduce effort where labels and identities are stable. Automatic machine evidence can strengthen timestamps and counts. Human confirmation remains necessary where acceptance, cause or disposition requires judgment.
Protect traceability through change
Rework, substitution, split batches, partial shipment and inter-plant transfer create the hardest cases. Treat each as a relationship rather than editing the original record until it looks simple.
If a batch is split, preserve parent and child identities. If material is substituted, record the affected quantity and approval. If output is reworked, link the new operation to the original defect and final release. If shipments combine several batches, retain the allocation.
History should show what actually happened, not what the route was supposed to be.
Measure retrieval and containment
Useful measures include:
- time to identify affected lots, batches and shipments;
- percentage of production with complete material and artwork identity;
- unreconciled quantity at control points;
- late or missing quality disposition;
- manual handoffs without acknowledgement;
- repeat jobs released without comparison;
- waste without job and reason;
- complaints where scope cannot be established.
Do not reward data volume. Reward decisions that become faster, safer and more precise because the evidence exists.
Build the minimum viable genealogy
Start with one important product family. Map the required backward and forward questions. Define identifiers, handoffs, units and exception rules. Test completed jobs before introducing more automation.
Where the chain breaks, decide whether the cause is unclear ownership, inconsistent master data, missing transaction or an impractical capture point. Fix the operating rule and then configure the tool.
Extend by risk and reuse. A stable core—order, version, material, batch, quantity, quality and shipment—can support increasingly detailed requirements without rebuilding the entire model.
Frequently asked questions
Design the exception routes
A clean production path is the easiest genealogy to demonstrate and the least useful test of resilience. Real control appears when work departs from plan.
Define how the record behaves when quantity is split, a material lot is substituted, output is transferred to another plant, an external supplier performs an operation, or held material is reworked. Each event should preserve the source identity, create the new relationship and reconcile quantity.
For a split, the parent batch remains the common origin while child quantities receive their own states and destinations. For rework, link the new operation to the defect, decision and output it attempts to recover. For substitution, retain the original requirement and the approved actual material. For consolidation, show every batch contributing to the shipment.
These relationships prevent the history from becoming a neat fiction. They also support proportionate response: only the child quantity processed under a suspect condition may need containment.
Make traceability useful every day
If genealogy is used only during an audit or complaint, people experience it as extra administration. Design daily benefits into the same evidence.
Warehouse can locate and allocate released material. Planning can see whether the exact job inputs are ready. Production can identify which revision and lot belong to a pallet. Quality can isolate a suspect batch. Customer service can explain shipment status. Finance can connect material and rework to actual cost.
When one scan or confirmation supports several decisions, capture quality improves naturally. Teams stop maintaining parallel notes because the shared record gives them something valuable in return.
Establish governance around identity
Someone must own product masters, material identities, revision rules, batch creation, unit conversion and retention. Otherwise integration connects fields whose meaning drifts over time.
Review duplicate items, missing lots, reused labels, impossible quantity balances and manual corrections. Treat these as process signals rather than IT housekeeping. A duplicate material code can widen a complaint investigation; a weak unit conversion can distort both stock and yield.
Publish simple rules and train at the handoff where each identity begins. Governance succeeds when operators understand the decision protected by the field, not when the data dictionary is merely complete.
Stage a two-hour trace exercise
Bring representatives from sales, purchasing, warehouse, prepress, production, quality and dispatch. Select one shipped pallet and one received material lot. Give the team two hours to trace both directions using normal access and records.
Record every pause, phone call, private spreadsheet and ambiguous identifier. Then rank gaps by customer risk and frequency. Some fixes may be small: adding the active artwork revision to a traveller, preserving lot identity on returned stock or acknowledging partial receipt at finishing.
Repeat after improvement with a more difficult case. The objective is not a perfect demonstration but a measurable reduction in the time and uncertainty needed to make a safe decision.
Does every individual carton need a unique serial number?
No. Choose unit, batch, pallet or shipment granularity according to product risk, customer need and process capability. The chosen level must still support credible containment.
Is barcode scanning the same as traceability?
No. Scanning captures an identity efficiently. Traceability depends on correct identities, relationships, quantities and decisions behind the code.
How far back should records be retained?
Retention should reflect contractual, regulatory, quality and commercial requirements. Define it by product and market rather than relying on inbox history.
Can mixed material lots be traced?
Yes, if every contributing lot and affected output batch is recorded. Mixed lots widen the possible affected population and should be used deliberately.
Where do ERP and MES fit?
ERP connects order, material, commercial and shipment structure. MES contributes execution evidence. Their value increases when both refer to the same job, batch, version and quantity.
Let the carton answer
A finished carton carries no visible account of the decisions that produced it. The factory must preserve that history on its behalf.
The work is not about recording everything forever. It is about preserving the few relationships that determine scope, responsibility and response when reality differs from plan. Those relationships should remain legible across departments, shifts, suppliers and years.
When the chain is connected, a customer question does not trigger an archaeological search. It triggers a controlled retrieval: this was the specification, this was the material, this was the process, this quantity was released, and this is the action now required.
That confidence protects response speed, customer trust and commercial judgment.