

The Order Is Still Open. Which Exception Will Break the Delivery First?
Garment delivery control improves when teams stop treating every open order as equally urgent and instead manage the few exceptions that can still break the promised date.
The short answer
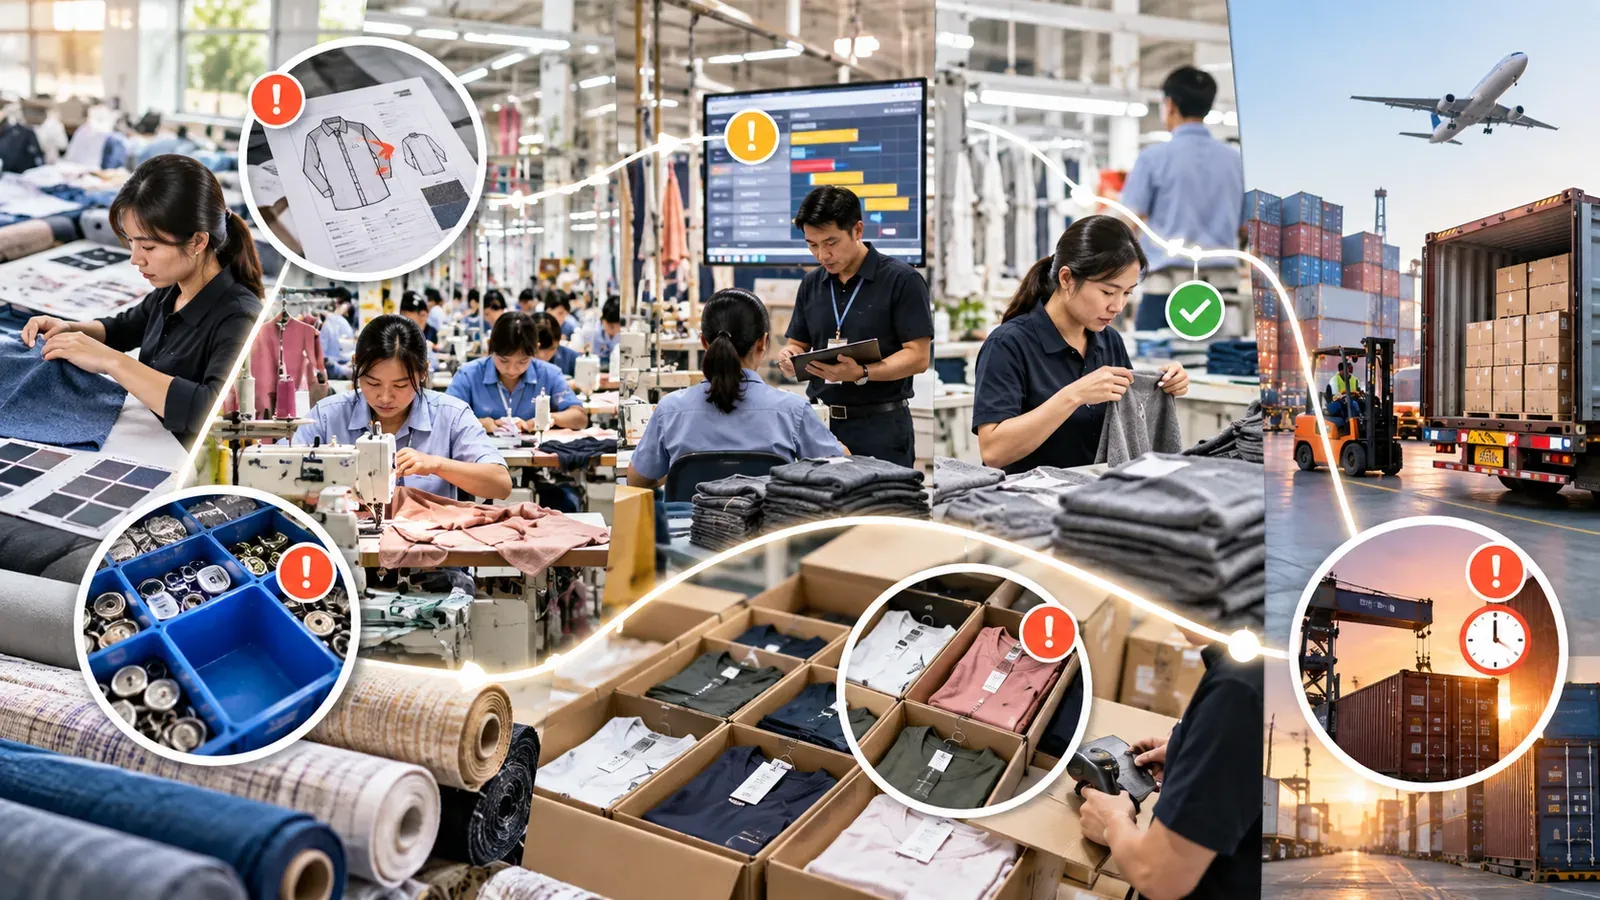
Most garment orders do not miss delivery because nobody knows the promised date. They miss because a small exception is allowed to stay invisible until it becomes a critical path problem. A trim remains unapproved, a buyer change reaches merchandising but not the line, a packing ratio is incomplete, an urgent order displaces two other orders, or a shipment is technically finished but not operationally ready for the cut-off. When every open order is shown with the same visual weight, management sees activity rather than risk.
The practical goal is therefore not to create a bigger order-status screen. It is to identify the few exceptions that can still change the delivery outcome, attach ownership and time to each one, and make the next operational decision obvious. That is where a garment-specific ERP/MES structure becomes useful: product, order, material, production, packing, shipping and finance need to describe the same order state instead of maintaining separate departmental truths.
Epicor Venus is designed around that connected garment workflow—from sample and order control to materials, production, shopfloor, shipping and finance. The important point is not the software label. The operating principle is that an exception should follow the order across functions, rather than disappearing at each handoff.
A long open-order list can hide the few orders that are actually in danger
An open-order list is usually factually correct and operationally weak. It may show order number, buyer, style, quantity, ex-factory date and perhaps a broad status such as “in production.” Those fields tell management what exists. They do not reliably tell management what is about to fail.
Consider two orders that both show 80% completion. Order A has all materials issued, stable buyer specifications, balanced size ratios, packing materials on hand and three working days before the shipping cut-off. Order B has 80% sewing completion but one color is behind, the care label artwork changed yesterday, cartons are not approved and the booking closes tomorrow afternoon. A conventional open-order report can make them look similar. Operationally they are completely different.
That gap matters because management attention is scarce. If the system does not surface the difference, teams compensate with chat groups, spreadsheets, phone calls and morning meetings. Those tools are useful for coordination, but they are poor substitutes for a shared operational state.
The first design principle is simple: status is not the same as risk.
The most dangerous delivery risk often appears between departments.
Garment manufacturing has many functional specialists. Merchandising controls buyer communication. Sourcing tracks fabric and trims. Planning allocates lines and capacity. Production manages output. Quality manages release. Warehouse and shipping manage packing, documents and dispatch. Finance closes the commercial result.
Most serious delivery problems occur between those areas rather than entirely inside one of them.
A buyer change may be acknowledged by merchandising but not reflected in material reservations. A replacement zipper may be ordered but not linked to the affected color-size combinations. Sewing may complete quantities that cannot form the required carton assortment. Shipping may receive a “finished” order that still lacks final carton dimensions or document approval.
This is why exception management should be modeled around cross-functional consequences. A useful exception record answers at least five questions:
- What changed or failed?
- Which order, style, color, size, material, line, shipment or buyer requirement is affected?
- What downstream date or operation is at risk?
- Who owns the next action?
- By what time must the action be completed before the delivery path changes?
Without those relationships, “exception management” becomes another list of alerts.
“Fabric available” is too weak a definition when the line is waiting
Fabric usually represents the largest material value, so it naturally dominates readiness discussions. But garment execution frequently stops on smaller items: a zipper puller, elastic, button, heat-transfer label, polybag warning, carton marking, hangtag or buyer-specific packing component.
A useful readiness view therefore cannot stop at “fabric in warehouse.” It needs to distinguish critical materials by the operation they gate. The most urgent missing item is not necessarily the most expensive item. It is the item whose absence prevents the next irreversible activity.
This is explored in Fabric Is Ready. Why Can One Missing Trim Still Hold the Whole Order?. The operational lesson is that material availability should be converted into order readiness, not treated as an isolated inventory fact.
A buyer change is only controlled when every affected team is acting on it.
Garment orders change constantly. Buyers revise color ratios, labels, trims, delivery splits, quantities, packaging or artwork. The risk is rarely that the company has no record of the email. The risk is that one team acts on the new instruction while another team continues from the old assumption.
A strong change-control flow creates a visible relationship between the buyer decision and every dependent object: sample/specification, BOM, purchase requirement, production instruction, packing rule, shipment plan and cost implication.
That does not mean every small change needs a committee. It means the system should make the blast radius visible.
The detailed article The Buyer Sent a Change. Did Merchandising, Planning and the Factory Act on the Same Decision? looks at the handoff between merchandising, planning and factory execution.
Finished sewing can still leave the order far from shipment-ready
Factories understandably celebrate sewing completion. But a commercial delivery is not finished when the last operation leaves the line. It is finished when the required units can be packed, identified, documented, released and handed over in the form the buyer and logistics plan require.
A classic example is assortment. The factory may have produced the total quantity, yet one size or color is short. The result is that the required carton ratio cannot be built. The missing quantity might be tiny in percentage terms and still block a large portion of the shipment.
That is why packing should be treated as another controlled transformation step, not simply the warehouse activity after production.
See Production Is Complete. Why Can Packing Assortment Still Delay Shipment? for the connection between color-size completion, carton building and actual shipment readiness.
Too much expediting can create the very delay it is trying to prevent.
Another common pattern is the “urgent order” effect. A buyer escalates. Management promotes the order. Planning changes the line sequence. Materials are moved. Supervisors switch style. Then another urgent request arrives.
Each individual decision may make sense, but the factory absorbs cumulative disruption: changeover time, learning-curve loss, partially completed bundles, displaced orders, reallocated trims and confused priorities.
The question is not whether priorities should ever change. Of course they should. The question is whether the cost of changing priority is visible before the decision is made.
One Factory, Too Many Urgent Orders. When Does Priority Switching Start to Hurt Delivery? examines how to distinguish a justified intervention from chronic expediting.
Shipping has a different clock from production
A shipment close to cut-off deserves a different level of control from an order six weeks away. But “close to cut-off” is still not enough. Shipping teams need to know whether the order is physically packable, whether the required quantity is released, whether cartons and labels are correct, whether documentation is complete, whether the booking exists, and whether the handover can happen within the remaining operational window.
industry guidance’s traceability model is useful conceptually because it separates events and the data required to describe them. In garment shipping, receiving, packing, shipping and transport are not interchangeable statuses. Each event has evidence.
The practical article The Vessel Cut-Off Is Friday. Which Order Exceptions Should Shipping Escalate First? focuses on this final execution window.
Management needs the few exceptions that can still change the outcome
The ideal management view is surprisingly small.
If a group has 200 open orders, the management team should not manually inspect 200 rows every morning. Most orders should remain invisible unless they cross a defined risk threshold. The system should elevate a manageable set of exceptions based on delivery impact, time remaining, material/production dependency, shipment constraint and recovery options.
That does not mean replacing judgment with an algorithm. It means giving judgment a better queue.
Management Sees 200 Open Orders. Which 10 Need Attention Today? takes that question into the management meeting: how the queue can move from status reporting to decisions.
The value is in cause, timing and recoverability—not another red status.
A garment exception model works best when it combines three dimensions.
Operational object. The exception must belong to something real: style, color, size, material, cut order, line, carton, shipment, buyer instruction or commercial order.
Time consequence. It must show the next date that becomes impossible if the issue is not resolved. A generic “late” flag is weaker than “trim approval required by 14:00 to preserve tomorrow's line start.”
Recovery decision. It should make alternatives visible: substitute material, partial shipment, line reassignment, overtime, split packing, buyer approval, alternate supplier or changed booking.
This is where connected data matters. If the system cannot connect the issue to those objects, teams will recreate the chain manually.
Where Epicor Venus helps management see the order that needs attention now
Epicor provides the enterprise-grade ERP foundation for purchasing, inventory, approvals, finance and governance. Epicor Venus adds garment-specific order, material, planning, production, packing and shipment context, allowing delivery exceptions to be understood across the full apparel flow rather than inside separate departmental reports.
That is where ACC's implementation role matters: defining which exceptions deserve escalation, what evidence management needs, and how the same order identity remains visible from material through shipment. Epicor Venus provides the industry layer while Epicor provides the enterprise backbone beneath the decision. Explore Epicor Venus for garment and apparel manufacturing.
Daily control should move attention to the order whose condition just changed
A useful rhythm is short and exception-led.
First, let normal orders stay normal. Do not force managers to review green work. Second, sort exceptions by the date they can still affect, not merely by how long they have been open. Third, require a named owner and next action. Fourth, record recovery decisions against the order so downstream teams see them. Fifth, close the exception only when the downstream condition is actually restored.
This is a very different behavior from updating a red/amber/green cell once a day.
The goal is not more reporting. The goal is fewer surprises.
Exception control works when the escalation is earlier than the failure.
A useful delivery exception should be defined around the next business gate that can still be protected. That gate may be material issue, line start, quality release, packing completion or logistics handover. The closer the order moves toward that gate, the less room remains for normal recovery. This makes time-to-gate a more meaningful priority signal than a generic overdue status.
The exception record should also show the operational dependency that failed. If the problem is a trim, management needs to know whether the component is awaiting supplier delivery, inspection, buyer approval or allocation. If the problem is production, the team needs to know whether the constraint is line capacity, rework, absenteeism or a sequence change. The root cause should remain attached to the order as it moves across departments.
Recovery choices should be explicit. The team may be able to substitute material, move the order, split the shipment, add overtime, change the booking or request buyer approval. Each option has consequences for cost, another order or the customer promise. Showing those consequences helps management choose deliberately instead of reacting to the loudest escalation.
Finally, the business should learn from closed exceptions. Track how early the warning appeared, when action was taken, which recovery option was selected and whether the order still met the commitment. Over time, the aim is fewer late surprises and earlier intervention. A mature exception process is not measured by how many alerts it generates; it is measured by how often the organisation still has practical choices when risk becomes visible.
The management challenge is deciding where intervention still has leverage
For The Order Is Still Open. Which Exception Will Break the Delivery First?, the final check is whether the current issue has a clear owner, a latest safe action time and an explicit downstream condition that proves recovery. That prevents the article's control logic from stopping at status reporting and keeps attention on the decision that can still change the result.
FAQ
Should every late task become a management exception?
No. Operational teams should resolve many issues locally. Management exceptions should be reserved for issues that threaten buyer commitment, cross departments, require resource trade-offs or need authority beyond the normal process.
Can an ERP predict every late order?
No. It can improve visibility, dependency tracking and prioritization, but judgment is still required. Unexpected machine problems, supplier behavior, buyer decisions and logistics constraints are not fully predictable.
Is MES enough for delivery exception control?
MES is valuable for shopfloor execution, but delivery risk can originate before or after production. A complete view also needs order changes, materials, packing, shipping and commercial context.
Why not manage exceptions in a spreadsheet?
A spreadsheet can be effective for a small temporary list. It becomes fragile when the data needs to stay synchronized with live orders, materials, line execution, packing and shipping events across many teams.