

From Sample to Shipment: Where Does Garment Manufacturing Lose Operational Control?
A practical framework for garment manufacturers to connect style, material, capacity, shopfloor and traceability decisions before small gaps become delivery problems.
The short answer
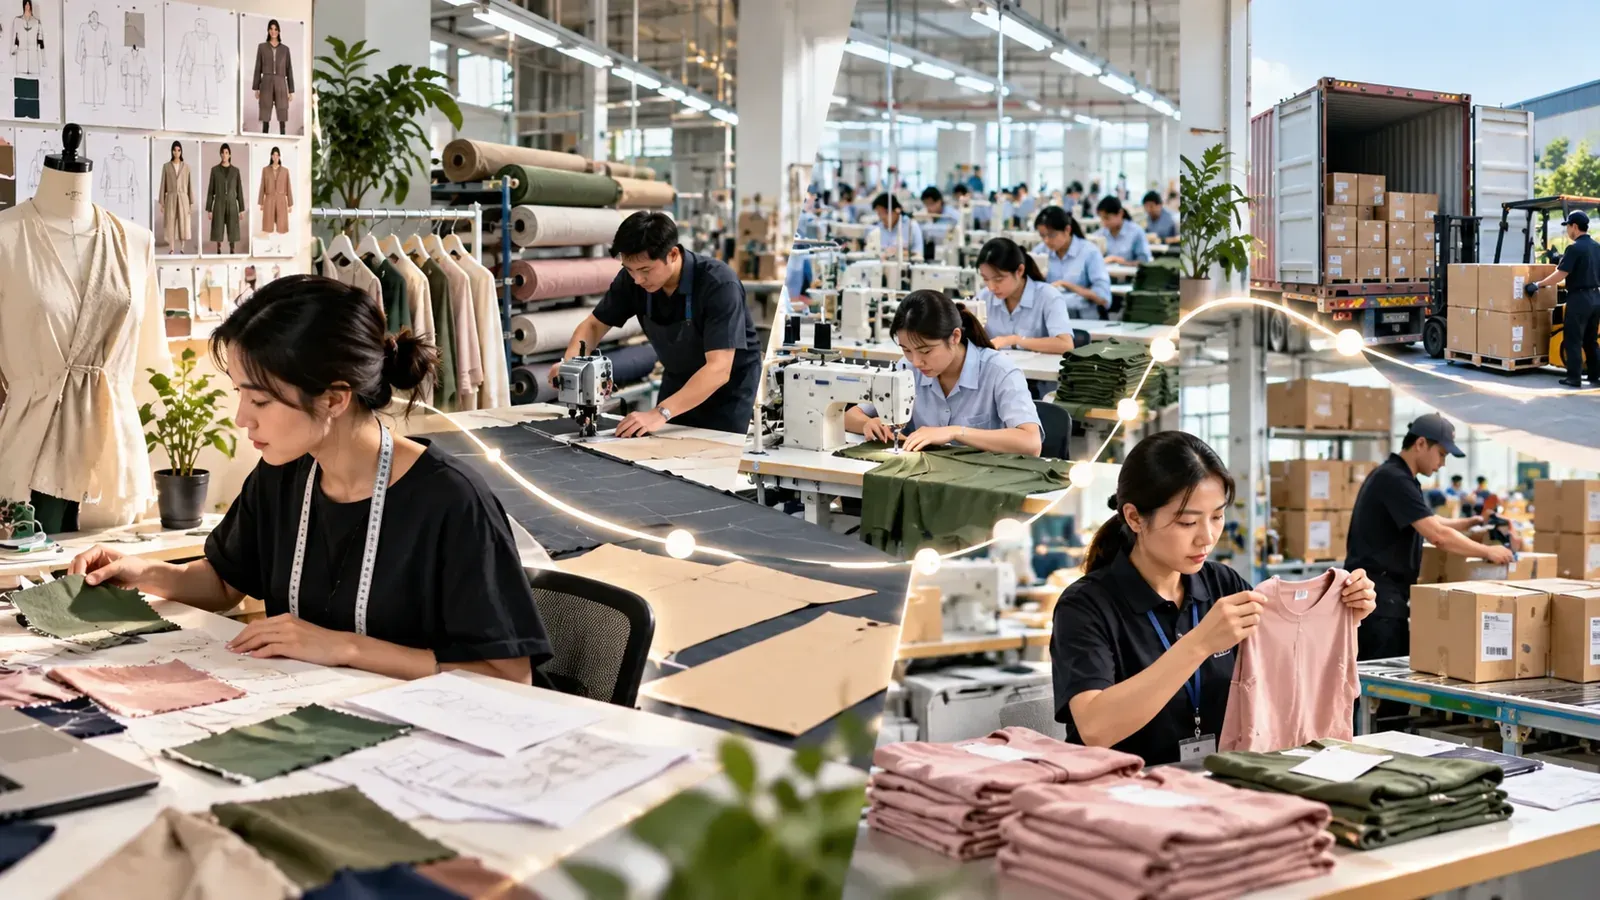
Garment manufacturing usually loses operational control not at one dramatic point, but in the handoffs between development, materials, planning, production and shipment. A sample can be approved while the production BOM still reflects an older revision. Fabric can be physically in stock while the rolls that meet width, shade or inspection requirements are not allocated to the order. Capacity can look sufficient in a weekly plan while changeovers, absenteeism, learning curves and late material release make the actual delivery window impossible. Shopfloor output can be reported every hour and still fail to answer the management question that matters: what is truly complete, what is blocked, and what decision must be made next?
The practical answer is to treat the style-order lifecycle as one connected control chain. Product identity, revision, material requirement, order commitment, capacity, WIP, quality and shipment evidence should refer to the same underlying style and order structure. The objective is not “more data.” It is fewer contradictory versions of operational truth.
That matters because apparel manufacturing is unusually sensitive to variation. A single style branches by color, size, destination, buyer requirement, factory and delivery window. Each branch can change consumption, material allocation, routing, quality requirements and shipment readiness. When those branches are managed in separate spreadsheets, messages and departmental systems, the business spends more time reconciling status than managing exceptions.
This article provides a management framework for finding the breaks. It also links to six deeper ACC Insights articles covering sample version control, BOM accuracy, fabric readiness, capacity planning, shopfloor WIP and textile Digital Product Passport readiness.
Why control is lost in the handoffs
A garment business is often described as a sequence: sample, cost, order, buy materials, cut, sew, finish and ship. Real operations are less linear. Buyers revise comments after costing. Material substitutions are approved after purchase orders are raised. Delivery windows move. One order may be split across factories. A line may start late because fabric passed quantity checks but failed shade grouping. Production reports may show pieces completed while quality holds prevent the same pieces from becoming available for packing.
The control problem therefore sits between functions. Each department may be doing its own job correctly while the end-to-end order still moves on the wrong assumption.
Three kinds of disconnect are especially common.
First is an identity disconnect. Teams are not referring to exactly the same style, version, color-size combination or order release. A style code exists, but the meaning attached to it has drifted.
Second is a timing disconnect. Information is correct but arrives after the dependent decision has already been made. A fabric shortage identified the morning before cutting is technically accurate information, but operationally it is late.
Third is an evidence disconnect. A status is reported without the supporting event or condition needed to trust it. “Fabric available” may not say whether it is inspected, allocated and physically at the right factory. “Production complete” may not say whether pieces have passed quality and are available for the next operation.
Garment-factory productivity improves through systematic process control rather than isolated fixes. Operational control becomes stronger when the business manages the full chain of dependencies instead of adding another report to one department.
Start with a stable style and order identity
A reliable operating model begins before bulk production. The style record must remain stable enough that development, costing, purchasing, planning and production know which version they are acting on.
This does not mean a style can never change. Apparel development is iterative by nature. The important distinction is between controlled change and uncontrolled ambiguity.
A controlled change has an owner, an effective version, a reason, affected materials or measurements, and a defined point at which downstream teams should stop using the previous version. An uncontrolled change lives in an email attachment, a buyer comment, a spreadsheet note or someone's memory.
Management should be able to answer:
- Which sample or specification version is currently approved for bulk?
- Which BOM version is effective for each color and size?
- Which open purchase orders were created before the latest change?
- Which production jobs or cut orders are affected?
- Has the change altered cost, consumption, delivery risk or quality checks?
The deeper article The Sample Was Approved. Why Is Production Still Working from the Wrong Version? examines this handoff in detail.
A garment BOM is a decision structure, not a flat list
The next break often appears in material planning. A garment BOM is rarely just “fabric, zipper, label, thread.” Color and size combinations change components. Trims may be buyer-specific. Packaging may vary by destination. A material substitution may be allowed for one colorway but not another. Consumption can move after marker or shrinkage assumptions change.
That is why BOM accuracy should be judged by whether it drives correct downstream decisions, not by whether a BOM screen exists.
A useful control test is to take one live order and trace a few combinations from style through requirement to procurement and allocation. Can the business show why a particular quantity of a particular component is required for a specific order release? Can it explain which assumption created the number? If a style revision changes one material, can planners see which demand and purchase commitments are affected?
The cluster One Style, Dozens of Color-Size Combinations. Where Does BOM Accuracy Break? focuses on this matrix problem.
Stock quantity is not the same as material readiness
Inventory is another area where a green number can be misleading. A warehouse may hold enough total metres of fabric, but the order can still be unready because the right rolls are not usable for the planned cut.
Readiness can depend on width, shade lot, shrinkage, inspection result, location, reservation, supplier status and whether the roll has already been allocated to another priority order. In multi-factory operations, the company can even have adequate group inventory but inadequate inventory at the site where the line is scheduled.
This is why “available stock” and “ready-to-cut stock” should be separate operational concepts. The second requires evidence that the material is fit, allocated and available at the point and time of use.
The cluster The Fabric Is in Stock. Why Is the Order Still Not Ready to Cut? provides a practical readiness checklist.
Capacity is only real when the dependencies are real
Planning systems can produce mathematically feasible schedules that fail in practice because the input assumptions are disconnected from current factory conditions.
Capacity depends on more than nominal machine or labor minutes. It is influenced by style complexity, operator skill, line learning, balancing, absenteeism, changeover time, rework, maintenance, feeding constraints and material release. Measures such as Standard Minute Value, throughput time, efficiency and productivity are useful only when the planning model and the actual execution model speak the same language.
A credible production plan should therefore distinguish between:
- theoretical capacity;
- demonstrated capacity for the style or operation mix;
- committed capacity already consumed by other orders;
- capacity exposed to material or approval risk;
- recovery capacity that management can realistically activate.
The cluster The Production Plan Fits on Paper. Why Does the Line Still Miss the Delivery Window? explores how to make that distinction operational.
WIP should describe flow, not just output
Many factories collect production output. Fewer have a WIP picture that reliably explains flow.
An output count answers “how many pieces were reported at this operation?” Management usually needs several additional answers: how many entered, how many passed, how many failed, where the bundles are now, how old the queue is, and whether the next operation can actually consume them.
That changes the role of shopfloor data. It becomes less about producing a daily summary and more about creating a chain of events that supports decisions during the shift.
Good WIP visibility should help a supervisor identify accumulating queues before end-of-day reconciliation. It should help planning understand whether a delayed operation is a local line problem or a symptom of material, quality or routing issues. It should let management distinguish a temporary reporting gap from a real production constraint.
The cluster Output Is Being Reported. Can Management Trust the WIP Picture? examines what makes shopfloor reporting decision-grade.
Traceability is moving from internal control to external evidence
Traceability is increasingly relevant beyond factory control. Emerging textile product-passport requirements are pushing manufacturers to connect product identity, material evidence, origin, compliance information and supply-chain events more consistently. Exact requirements can continue to evolve, so the most durable preparation is better connected operational data.
For garment manufacturers, the useful management question is not “Which QR code should we print?” It is “Can we reliably assemble the product and supply-chain evidence that a future passport may require?”
That evidence may involve product identity, fiber or material information, origin, supporting compliance documents and traceability links. The architectural lesson is to use stable identifiers and structured event data so information can move across systems and partners without creating another disconnected database.
The cluster Digital Product Passports Are Coming for Textiles. Is Your Garment Data Ready? explains why DPP preparation should begin with data architecture rather than presentation.
A practical control model: seven questions for one live order
Management can test operational control without launching a transformation project. Pick one important live order and ask seven questions.
1. Which version are we making?
The approved sample, specification, measurement, BOM and order requirements should point to the same effective revision.
2. What exactly must be available?
Material demand should be explainable by style, color, size, quantity, consumption logic and approved substitutions.
3. Is the material ready for this factory and this cut?
Do not stop at total inventory. Check inspection, allocation, shade/lot constraints, physical location and required date.
4. Is the capacity assumption demonstrated?
Compare planned minutes with recent performance for similar work, current staffing, changeover and bottleneck conditions.
5. Where is the order now?
The answer should be based on operation-level evidence, not a manually consolidated end-of-day estimate.
6. What is preventing the next milestone?
Every red or amber status should resolve to a specific exception with an owner and next action.
7. Can the company reconstruct the evidence later?
Product identity, material source, production events, quality evidence and shipment information should be retrievable without rebuilding the story from inboxes.
If managers cannot answer one of these questions quickly, the problem is not necessarily that the company needs more software. It means the operating model has a break in ownership, data structure or event capture.
What connected control changes
A connected ERP/MES environment changes the sequence of management work. Instead of departments periodically sending status to a central coordinator, the underlying transactions create a shared operational state.
For example, an approved sample version can become the basis for costing and BOM control. The order can drive material requirements and production demand. Material receipts, inspection and allocation can change readiness. Production events can update WIP. Quality and shipment milestones can close the order lifecycle. Finance can then consume the same operational records instead of reconciling separate spreadsheets.
This is the context in which Venus is relevant. ACC positions Venus as a garment-focused ERP, MES and AI platform covering sample management, multidimensional BOM, fabric planning, production, shopfloor execution and multi-factory coordination. The useful management point is not that one platform automatically fixes weak processes. It is that garment-specific structures can reduce the number of translation points between development, planning and execution.
A system should make exceptions more visible, not simply make transactions digital.
What management should measure
A control model needs measures that reveal decision quality, not just departmental activity. Useful measures include:
- percentage of production orders released on the correct approved revision;
- material-readiness accuracy at the promised cut-release date;
- number and age of unresolved material exceptions;
- plan-versus-actual start date by line and style;
- throughput time between key operations;
- WIP age at constraint operations;
- rework or hold quantities not yet reflected in planning;
- number of manual status reconciliations required before the daily production meeting;
- percentage of traceability evidence retrievable from structured records rather than email or shared folders.
The objective is to reduce the time between an operational fact becoming true and management being able to act on it.
Frequently asked questions
Does end-to-end visibility mean every department must use one screen?
No. Different roles can use different interfaces. The important requirement is that the screens refer to the same style, order, material and execution records rather than separate copies of status.
Should garment manufacturers start with ERP or MES?
It depends on the control gap. If style, BOM, order and material structures are inconsistent, adding faster shopfloor data will not solve the upstream problem. If master and planning data are already reliable but execution remains opaque, MES may be the immediate constraint. The architecture should connect both.
Is real-time data always necessary?
No. The required frequency depends on the decision. A line supervisor may need intrashift WIP signals; finance may not. “Real time” only adds value when someone can act at that speed.
How does this relate to Digital Product Passports?
DPP readiness depends on reliable product identity and supporting supply-chain evidence. A company with fragmented style, material and traceability records will find passport preparation harder even if the final DPP interface is simple.
What should management fix first?
Choose a high-value order and identify the earliest point where teams disagree about status or version. Fix that handoff before adding more dashboards. Operational control improves when the same evidence survives from one decision to the next.