

You Already Have the Die and Plates. Are They Still the Right Tools for This Revision?
Reusable dies, plates, cylinders and tooling save time only when teams know which customer, artwork and specification revision each tool represents. Weak tooling control can reproduce an obsolete job perfectly.
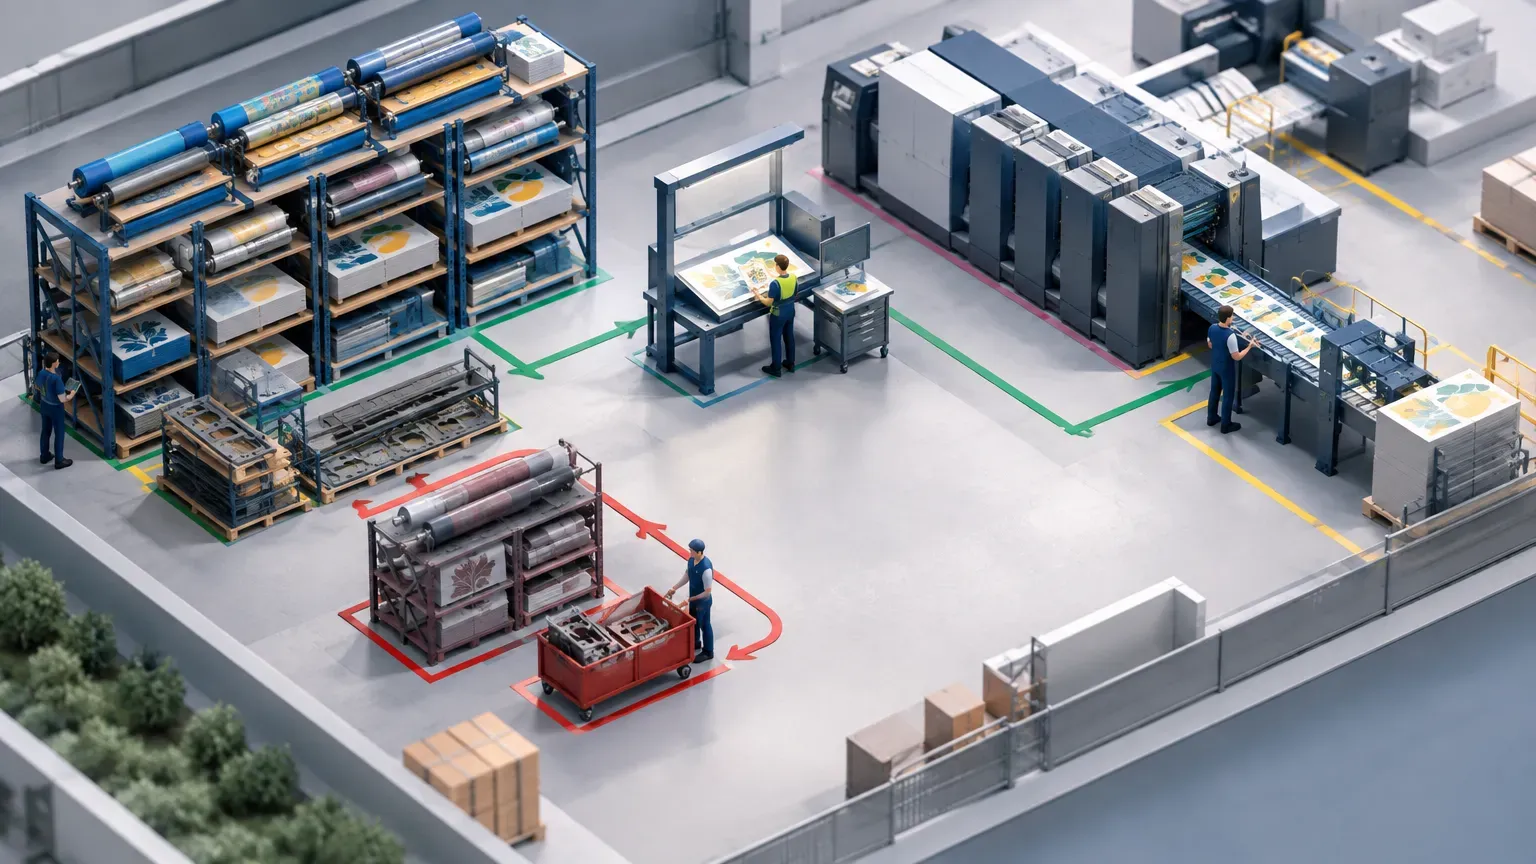
The short answer
Reusable plates, dies, cylinders and other production tools should be linked to the exact job specification and revision they represent. Tool availability is useful only if the business can confirm that the tool is still technically and commercially valid for the current customer requirement.
A stored tool can be in perfect physical condition and still be wrong.
How this connects to the pillar
The broader job-change model is covered in The Customer Changed the Job Again. How Do You Keep Specs, Cost and Production Aligned?. Tooling control ensures that a new job revision does not accidentally inherit an obsolete production asset.
Reuse creates value and risk
Tooling reuse can reduce setup time and cost.
But the more tools a plant keeps, the more important identity becomes.
A die may look nearly identical to another. Plates may represent different language or promotional versions. Cylinders may have small artwork changes. Screens or embossing tools may correspond to customer-specific revisions.
The physical tool needs a controlled digital identity.
Link tool identity to revision
Useful tooling records can include:
- tool ID;
- customer;
- product;
- job or specification;
- artwork revision;
- dimensions;
- creation date;
- status;
- storage location;
- inspection condition;
- superseded-by relationship.
The exact fields depend on the process.
The important rule is that the tool can be validated against the current job before it is issued.
Separate physical condition from revision validity
Inspection answers: can this tool still run?
Revision control answers: should this tool still run for this job?
Both are required.
A well-maintained die may have the wrong dimensions after a carton change. A plate can be undamaged but show an old barcode.
Tooling release should therefore consider condition and version.
Make tool selection part of job preparation
Do not wait until the press or finishing machine is ready to discover that tooling is uncertain.
Job preparation should verify the required tools against the current revision.
If a new tool is needed, planning should know before the scheduled setup.
This improves both schedule reliability and change-cost visibility.
Capture remake reason
When tooling is remade, record why.
Possible reasons include:
- customer artwork change;
- dimension change;
- damage;
- wear;
- process improvement;
- wrong original output;
- supplier issue;
- tooling lost or unavailable.
The reason matters to costing and continuous improvement.
A customer-driven remake should not be analyzed the same way as avoidable internal damage.
Retire obsolete tooling deliberately
Old tools can create accidental reuse.
If a revision makes a tool invalid, change its status.
Depending on the business, the tool may be destroyed, quarantined, archived or retained for reference.
The status should prevent normal production selection.
Physical labeling should support the system status rather than contradict it.
Manage families of similar tools
Packaging businesses often maintain many tools for related sizes or designs.
A structured hierarchy helps distinguish:
- common base design;
- size variant;
- language or artwork variant;
- customer variant;
- revision.
This reduces reliance on tribal knowledge.
It also helps planners understand whether a new job truly needs new tooling.
Connect tooling to costing
Tooling cost can be:
- charged to the customer;
- amortized;
- absorbed by the business;
- reused across repeat jobs.
The job should reflect the commercial model.
When late revision makes existing tooling obsolete, capture the new cost and the reason.
That evidence supports both margin analysis and customer change discussions.
Use tooling history for repeat jobs
A repeat order should not simply retrieve the last tool automatically.
First confirm that the current specification still matches the tooling revision.
Then check condition and availability.
This small validation prevents the efficiency of repeat production from becoming a version-control risk.
What management should measure
Useful indicators include:
- tooling remakes;
- remake reason;
- obsolete tools still active;
- jobs delayed by missing tooling;
- tools issued against superseded revisions;
- tooling damage;
- tooling cost caused by customer change;
- duplicate tools created because existing assets could not be found;
- repeat jobs requiring new tooling unexpectedly.
These measures show whether tooling is an asset library or a hidden source of risk.
ACC and Jupiter context
Jupiter is built around printing and packaging jobs where specifications, production operations and costing need to remain connected. Linking reusable tooling to the controlled job revision helps the business gain the economic benefit of reuse without losing version certainty. Explore Jupiter for printing and packaging.
Operational review point
Select ten frequently reused tools.
For each one, ask whether the plant can identify:
- what customer/product it belongs to;
- what revision it represents;
- whether it is still valid;
- where it is stored;
- when it was last inspected;
- which recent jobs used it.
Any answer that depends only on one experienced employee is a useful improvement target.
Control modified tooling
Some tooling can be altered rather than replaced.
If a die, plate or other tool is modified, update the revision relationship so the physical asset and digital record remain aligned.
A modified tool should not continue to carry an identity that implies the old geometry or artwork is still present.
Include tooling availability in scheduling
A job may have material and machine capacity but still be unable to run because a required tool is at another site, with a supplier, under repair or waiting for remake.
Tooling readiness should therefore become part of job preparation for processes where the tool is critical to start.
Verify tooling at issue and return
Tooling control improves when issue and return are treated as operational events.
Before issue, confirm the tool matches the job revision and is fit for use.
On return, record condition, storage location and any damage.
This creates a reliable lifecycle around high-value reusable assets.
Manage duplicate tooling deliberately
Sometimes duplicate tools are justified for volume, backup or multi-site production.
The business should know that duplicates exist and whether they are equivalent.
Two tools with the same job reference may have different revision, wear history or modification status.
Duplicate does not mean interchangeable unless the record confirms it.
Connect tooling to maintenance history
For high-use dies, cylinders or other tooling, wear can gradually affect output.
Inspection and maintenance history can help distinguish process problems from tooling condition.
If the same defect recurs on jobs using one tool, the history provides a useful investigation path.
Include external tooling custody
Tools may be stored with subcontractors or specialist suppliers.
The business still needs visibility of ownership, revision, condition and location.
When the job is repeated, planners should know whether the tool is immediately available or must be retrieved, checked or remade.
This prevents external custody from becoming invisible schedule risk.
Standardize retirement decisions
When a product is discontinued or a revision becomes obsolete, define what happens to the associated tools.
Some may be destroyed for confidentiality. Some may be retained for historical or service requirements. Some may be modified.
A consistent retirement rule reduces clutter and accidental reuse.
Use tooling genealogy for revised families
When a new tool is derived from an existing one, record that relationship.
Knowing that die B was created from die A after a dimension change, or that plate set C superseded plate set B after a copy revision, helps teams understand why several similar tools exist.
Genealogy also supports investigation when a repeat job unexpectedly behaves differently.
Separate customer-owned and company-owned tooling
Ownership affects retention, charging, disposal and transfer.
A customer-owned die may need different approval before destruction or modification. Company-owned tooling may be managed under internal reuse policy.
Record ownership clearly so operational decisions do not create commercial disputes.
Review storage design as part of tooling control
Good data does not help if physical storage makes the wrong tool easy to pick.
Use locations, labeling and quarantine areas that support the system status.
Obsolete or damaged tools should not sit in the same normal-pick location as active tooling if that creates selection risk.
Include tooling verification in first-off approval
Where practical, confirm the correct tooling during setup or first-off inspection.
This creates a final physical check before the full run begins.
The verification can be simple, but it should confirm revision identity rather than relying solely on visual familiarity.
Frequently asked questions
Should old dies or plates always be destroyed?
Not necessarily. The business may retain them for reference or future authorized versions, but obsolete tools should be clearly controlled against accidental use.
Is a tool ID enough?
Only if the ID is connected to the current job/specification relationship and users can verify it before production.
Should tooling remake cost be tracked separately?
It is useful when the reason matters commercially or operationally, especially for customer revisions, damage and avoidable remake.
Can repeat orders use the previous tooling automatically?
They should first confirm that the current artwork and specification still match that tool revision.