

The First Sheet Looks Good. What Must Be Approved Before the Run Continues?
First-off approval should confirm more than appearance. It must establish the version, material, colour, registration and process conditions that make the result repeatable for the full run.
The short answer
First-off approval should confirm more than appearance. It must establish the version, material, colour, registration and process conditions that make the result repeatable for the full run.
First-off approval converts a plan into physical evidence
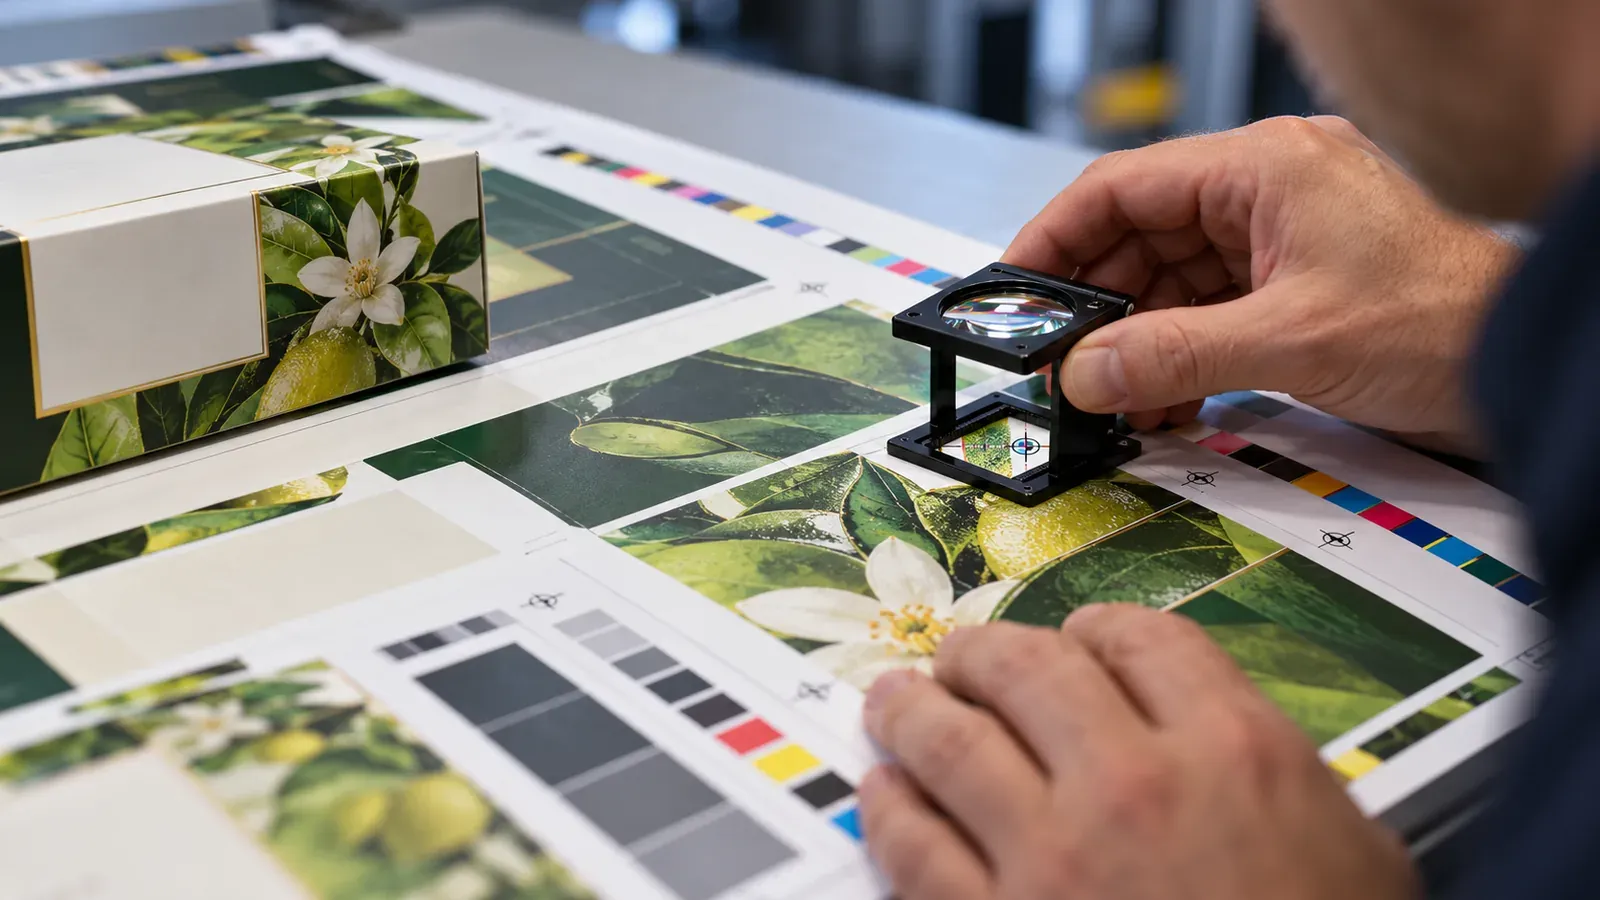
Before the run, the factory has artwork, specifications, standards and settings. The first acceptable sheet or unit is where those elements are proven together. It should show that the correct version is running on the intended substrate, with acceptable colour, registration, image content and critical dimensions. If approval checks only whether the sheet looks generally acceptable, important assumptions remain unverified. A disciplined gate defines the characteristics that matter for that job and records the conditions under which the approval was granted.
Version identity must be unambiguous
Packaging jobs often contain similar language versions, SKU variants or late artwork changes. A visually attractive first sheet can still be wrong if the version is not the one released for production. The approval step should confirm the job, artwork revision and any variable content before the run is allowed to continue. This is especially important when plates, cylinders, files or gang layouts contain multiple items. Version control is therefore a quality control, not merely a document-management task.
Material identity belongs in the approval record
The accepted appearance depends on the substrate. A different paper shade, board surface, film or coating can change colour and downstream behaviour. First-off approval should therefore verify the allocated material and, where relevant, its batch or lot. If production changes to another batch later, the team can decide whether the difference is within normal limits or whether a new check is needed. This prevents the approved standard from being separated from the physical input that produced it.
Colour and registration need explicit acceptance criteria
Terms such as “looks good” are too vague for a long run. The team should know which colour references, density targets, registration points or visual tolerances apply. The exact measurement method will depend on the job, but the decision rule should be understood by the operator and quality team. A clear standard also reduces disagreement when the process drifts. Instead of debating preference, the team can compare current output with the approved reference and defined tolerance.
Approval conditions should survive shift changes and restarts
A job may continue across multiple hours, shifts or machines. The person who approved the first sheet may not be present later. Recording the relevant setup and reference conditions allows the next team to reproduce the accepted state rather than start from memory. Long stops, plate changes, material changes or major adjustments should trigger a defined re-verification rule. That keeps first-off approval active throughout production instead of treating it as a one-time event.
The gate should be fast but not casual
A quality gate that takes too long creates pressure to bypass it; a gate that is too casual creates rework. The practical design is to check a short list of high-risk characteristics, capture approval evidence and release the run immediately when those conditions are met. Low-risk repeat jobs may need a lighter check than a new structural pack or difficult colour job. Risk-based approval keeps control proportional without turning every makeready into paperwork.
Link the approval decision to the wider quality system
First-off approval is one control point within the broader printing and packaging quality-control workflow. When later defects appear, the team should be able to compare them with the first accepted result and determine what changed after release. That evidence shortens root-cause analysis and helps distinguish a pre-existing setup issue from drift during production.
Measure whether first-off control is preventing waste
Useful measures include first-off rejection rate, time to approval, number of adjustments before release, restart re-approval frequency and defects discovered after the approved point. If approval is consistently fast but downstream defects remain high, the checklist may be missing a critical characteristic. If approval takes too long, the standard or process capability may need attention. The aim is a stable gate that catches meaningful risk early without becoming a production bottleneck.
Define who has release authority
Approval ownership should be explicit. The press operator may prepare the sample, quality may verify specified characteristics, and production management may control schedule release. The exact model can vary, but everyone should know who can stop, who can approve and what happens when the result is borderline. Clear authority prevents the common situation where production continues because nobody wants to make the decision to hold it.
Keep retained references usable
A retained approved sheet or sample is valuable only if it can be identified and preserved. Store the job and version reference with it and protect it from fading, contamination or mix-up. For repeat work, the retained sample should support comparison but should not override a newer customer-approved standard. The reference is evidence, not an uncontrolled substitute for current specifications.
Practical management checklist
- Confirm the current released version and material before action.
- Define the characteristic that must be accepted or corrected.
- Record affected quantity and process location.
- Assign one owner for containment and one decision for release.
- Keep the evidence attached to the job for post-job review.
What management should measure
For printing first off approval, management should track the frequency of exceptions, the quantity placed on hold, rework or scrap created, time to containment, and recurrence of the same cause. Trend these measures by job type and process so that the business can distinguish an isolated event from a weak operating standard. The useful question is not whether every variation can be eliminated; it is whether the control system is finding important variation early enough to prevent repeated loss.
Operational review point 1
For operational review point 1 in this printing first off approval topic, management should review the live job at the moment when evidence changes rather than waiting for final closure. Compare the released specification, current material and process condition, quantity at risk, downstream consequence and customer commitment. If the condition is outside the agreed standard, record the containment decision and the owner responsible for returning the job to a controlled state. This creates a practical bridge between quality evidence and production action, while preserving enough context for post-job learning without adding unnecessary reporting steps.
At review point 1, the team should also ask whether the exception is genuinely unique or resembles a previous event. If the same cause appears across similar jobs, the response should move beyond one-off correction and update the relevant operating standard, preventive check or planning assumption. That is how a quality system becomes progressively more stable rather than repeatedly solving the same issue under different job numbers.
Operational review point 2
For operational review point 2 in this printing first off approval topic, management should review the live job at the moment when evidence changes rather than waiting for final closure. Compare the released specification, current material and process condition, quantity at risk, downstream consequence and customer commitment. If the condition is outside the agreed standard, record the containment decision and the owner responsible for returning the job to a controlled state. This creates a practical bridge between quality evidence and production action, while preserving enough context for post-job learning without adding unnecessary reporting steps.
At review point 2, the team should also ask whether the exception is genuinely unique or resembles a previous event. If the same cause appears across similar jobs, the response should move beyond one-off correction and update the relevant operating standard, preventive check or planning assumption. That is how a quality system becomes progressively more stable rather than repeatedly solving the same issue under different job numbers.
Frequently asked questions
Is final inspection enough for printing and packaging quality?
No. Final inspection can detect problems, but it cannot recover the time and material already consumed. The stronger approach is to place controls at the process stages where important characteristics are created or can change.
Should every small variation stop production?
No. Teams need defined tolerances and escalation rules. Normal variation can continue within control limits, while material deviations, wrong versions, significant process drift or critical defects require containment and review.
How does traceability help quality improvement?
Traceability connects the defect to the actual version, material, process event and shipped quantity. That shortens investigation and helps management correct the real source instead of relying on assumptions.
What should happen after rework is completed?
The current job should be verified and released, but the cause should also be reviewed. If the issue is recurring or systemic, the relevant standard, workflow or preventive control should be changed.