

Paper Is in Stock. Why Is the Press Still Waiting?
Inventory availability is not the same as production readiness. A printing job can wait even when paper or board is physically in stock because specification, quantity, preparation or companion materials are not ready.
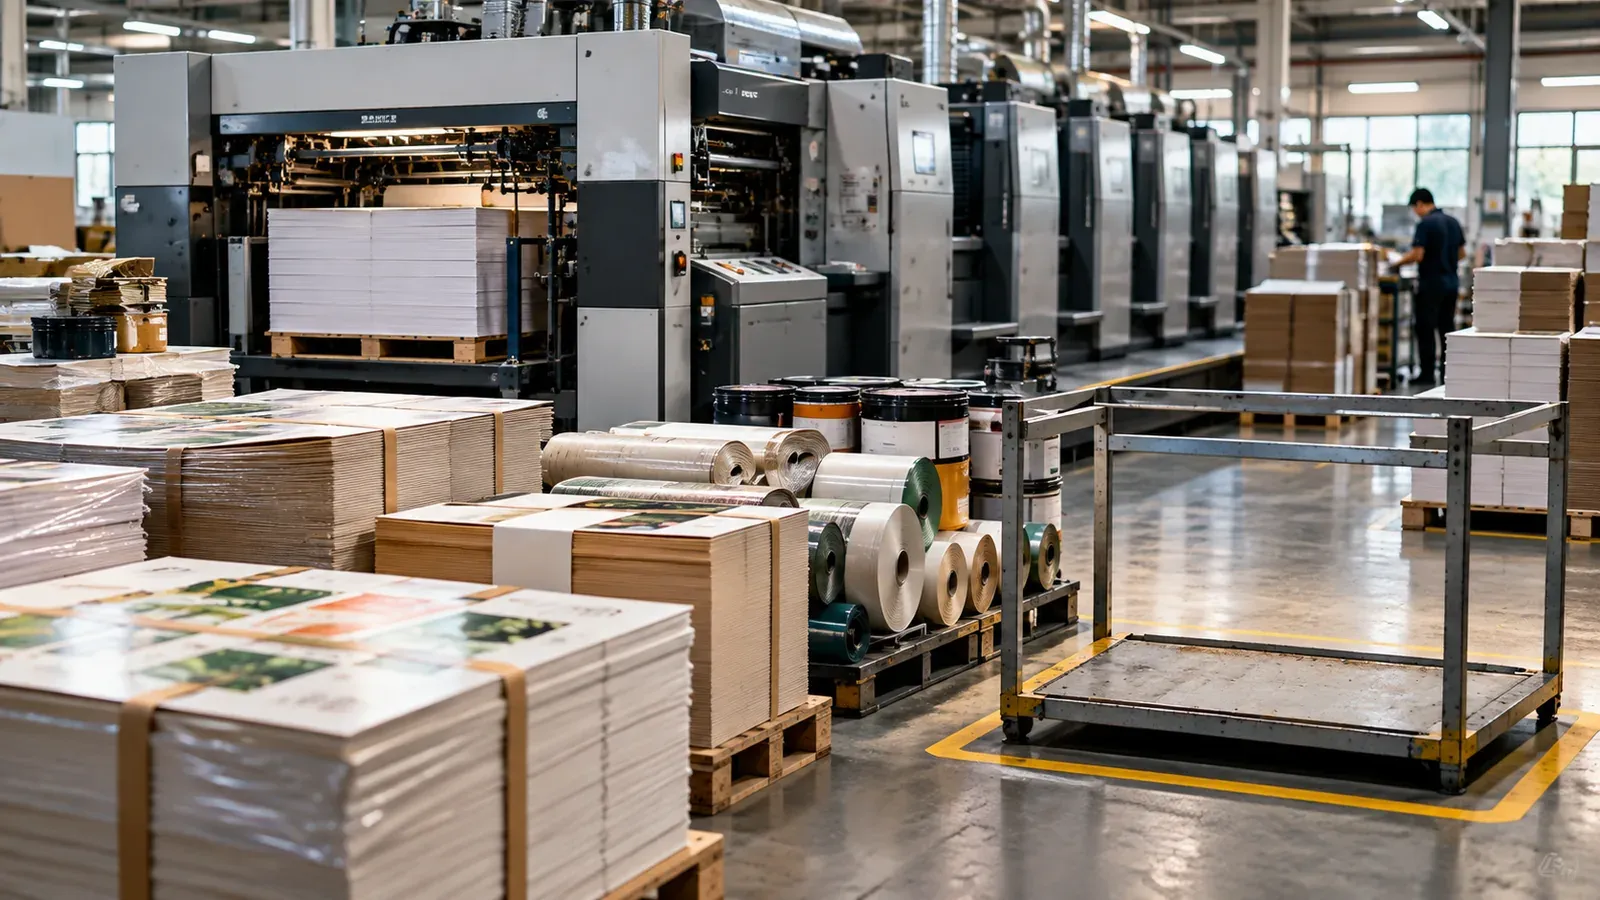
The short answer
A stock balance can say the material is available while the press still cannot start the job. For printing and packaging, true readiness depends on more than quantity. The correct grade, size, grain, coating, batch, roll condition, certification, ink, plate, tooling and staging status may all matter. Planning improves when “in stock” and “ready for this job at this time” are treated as different states.
Inventory availability answers the wrong question
Inventory tells you what the business owns. Production readiness asks whether the required material can be consumed by the planned operation now. A warehouse may hold enough total board but not enough in the correct size, batch or finish. A roll may exist but still require slitting. Sheets may need conditioning or inspection. When planners use inventory quantity as a proxy for readiness, the schedule can reserve a press slot around material that is not actually executable.
Specification matters as much as quantity
Substrate properties influence printability, colour, dimensional stability, finishing and customer acceptance. Substitution therefore needs control. A material that looks commercially equivalent may behave differently on press or in die-cutting and folding. Before substituting, the business should identify which technical and customer requirements are affected and whether the change alters cost, waste or approval status.
Companion materials can stop the whole job
Paper is highly visible, but a job may also depend on ink, coating, foil, adhesive, plates, blankets, tooling, packing material or externally supplied components. One missing companion item can make the main substrate irrelevant. A material-readiness check should therefore be job-based rather than item-based: all critical components required for the next operation must be ready together.
Reserved material is not the same as physically staged material
System allocation protects quantity from being consumed by another job, but the press also needs the material at the right location and condition. Warehouse picking, movement, acclimatization, slitting, cutting, inspection and line-side staging can take time. If those preparation steps are not included in the schedule, the press may wait for material that was technically reserved hours earlier.
Readiness should have a timestamp
A useful material status is not simply ready/not ready. Planners need to know when the job will become ready relative to the planned setup. A supplier delivery at noon does not support an 08:00 press start, and a warehouse release at 08:00 may still be too late if preparation requires two hours. Time-phased readiness allows planners to move jobs before a machine is idle rather than discover the problem at setup.
Exception management reduces last-minute expediting
The most useful material report is not a full list of inventory. It is the list of scheduled jobs whose required materials are not expected to be ready by the preparation cutoff. Those exceptions can be resolved through substitution, resequencing, supplier follow-up, partial production or a revised promise. Management should focus on the gap between the production schedule and the material-readiness plan.
Material readiness affects margin as well as delivery
Waiting creates labour and machine inefficiency, while emergency substitution can increase purchase price or waste. Split deliveries and urgent freight add further cost. A material problem is therefore both a service issue and a margin issue. Recording the reason for delay helps distinguish supplier, planning, warehouse and specification causes and feeds better assumptions into future quotations.
A practical readiness gate before press release
Before confirming the press slot, check specification, available and reserved quantity, quality status, required preparation, companion materials, plates/files, tooling and staging completion. Define a cutoff by which those elements must be confirmed. If the gate is not met, the planner should have authority to resequence work rather than preserve a schedule that the factory cannot execute.
How Jupiter fits the workflow
ACC — Jupiter Printing & Packaging ERP connects material planning, production scheduling, BOM/routing logic and shop-floor visibility for print and packaging operations. The management value is the ability to align material readiness with the actual production sequence instead of checking stock and machine calendars separately.
Related ACC Insights
- Why Printing and Packaging Jobs Lose Margin Between Quote and Shipment
Management checklist
- Confirm the current job assumption that management is relying on.
- Compare the planned condition with the latest operational evidence.
- Identify whether cost, capacity, quality or delivery commitment has changed.
- Assign an owner and decision time for material exceptions.
- Keep the reason for the decision attached to the job for post-job learning.
Define readiness by the next operation, not by purchasing status
A purchase order marked received does not mean a press-ready job exists. The substrate may still require inspection, conditioning, slitting, allocation or movement to the correct staging area. Ink, coating, foil, adhesive, plates or outsourced components may be incomplete. The practical definition of readiness is therefore operation-specific: can the next scheduled operation start at the planned time with the correct approved inputs physically available?
That definition should be visible before the press slot begins. A simple readiness gate can cover substrate, ink or consumables, approved artwork and plates, tooling, operator requirement, quality instructions and downstream route. If one critical item is missing, the job should be identified as constrained rather than left on the schedule as if it were fully executable.
Measure the cost of late readiness, not only stock availability
Inventory reports answer whether material exists. Production control needs a different measure: how often did a scheduled job fail to start because an input was not ready at the required place and time? Recording that reason exposes the hidden cost of moving jobs, repeating setup decisions and leaving expensive equipment idle.
The pattern matters. Repeated substrate shortages point toward planning parameters or supplier reliability. Repeated plate or proof delays point toward release discipline. Repeated internal staging failures point toward warehouse-to-press execution. Without reason codes, all three may appear as a generic schedule miss even though the management response is different.
Create a freeze window for the next press horizon
One practical approach is to protect a short forward horizon: for example, the next shift or the next several jobs on a critical press. Jobs entering that window should have passed the readiness gate. If they have not, the planner either resolves the constraint or substitutes another genuinely ready job before the gap becomes an emergency.
This reduces the temptation to use nominal inventory or a planned purchase date as proof that the schedule is safe. It also gives purchasing and prepress a clear priority list because they can see which missing input threatens the next committed production sequence.
Material readiness is one component of the wider job-control chain. Why Printing and Packaging Jobs Lose Margin Between Quote and Shipment explains how readiness, capacity, execution and downstream completion need to remain connected to the original commercial assumptions if management wants to protect both delivery and margin.
Distinguish shortage from allocation failure
A material can be physically present in the building and still be unavailable to the job. It may be reserved for another order, waiting for inspection, stored in the wrong location or not converted into the required size. Treating all of these conditions as “in stock” hides different corrective actions. The readiness check should therefore confirm both existence and allocation: the required quantity must be released to the specific job and able to reach the operation before setup begins.
Stage the next job before the current run finishes
Readiness becomes more reliable when the next job is physically staged while the current press run is still active. Material, plates, consumables and instructions can then be checked against the released job before the machine becomes available. This simple overlap moves problem discovery earlier. Instead of finding a shortage during makeready, the team has time to locate, substitute or resequence before valuable press capacity is exposed.
Frequently asked questions
Why can the press wait when paper shows as available?
Because available quantity may not be in the required specification, size, condition or location, or other critical materials may still be missing.
What is a material-readiness gate?
It is a defined check before production release that confirms all critical job materials and preparation steps will be ready by the required start time.
Should material be staged before the press slot?
Yes. The staging lead time should reflect picking, movement, inspection, cutting or slitting, and any conditioning needed before use.
How does material readiness affect job cost?
Waiting, substitution, extra handling, waste and expediting can all increase actual cost even if the purchase price of the main substrate stays within budget.