

The Paper Was Right. The Lot Was Wrong.
A substrate can match its commercial description yet behave differently by lot, condition, coating or storage history. Traceability makes that variation actionable.
The short answer
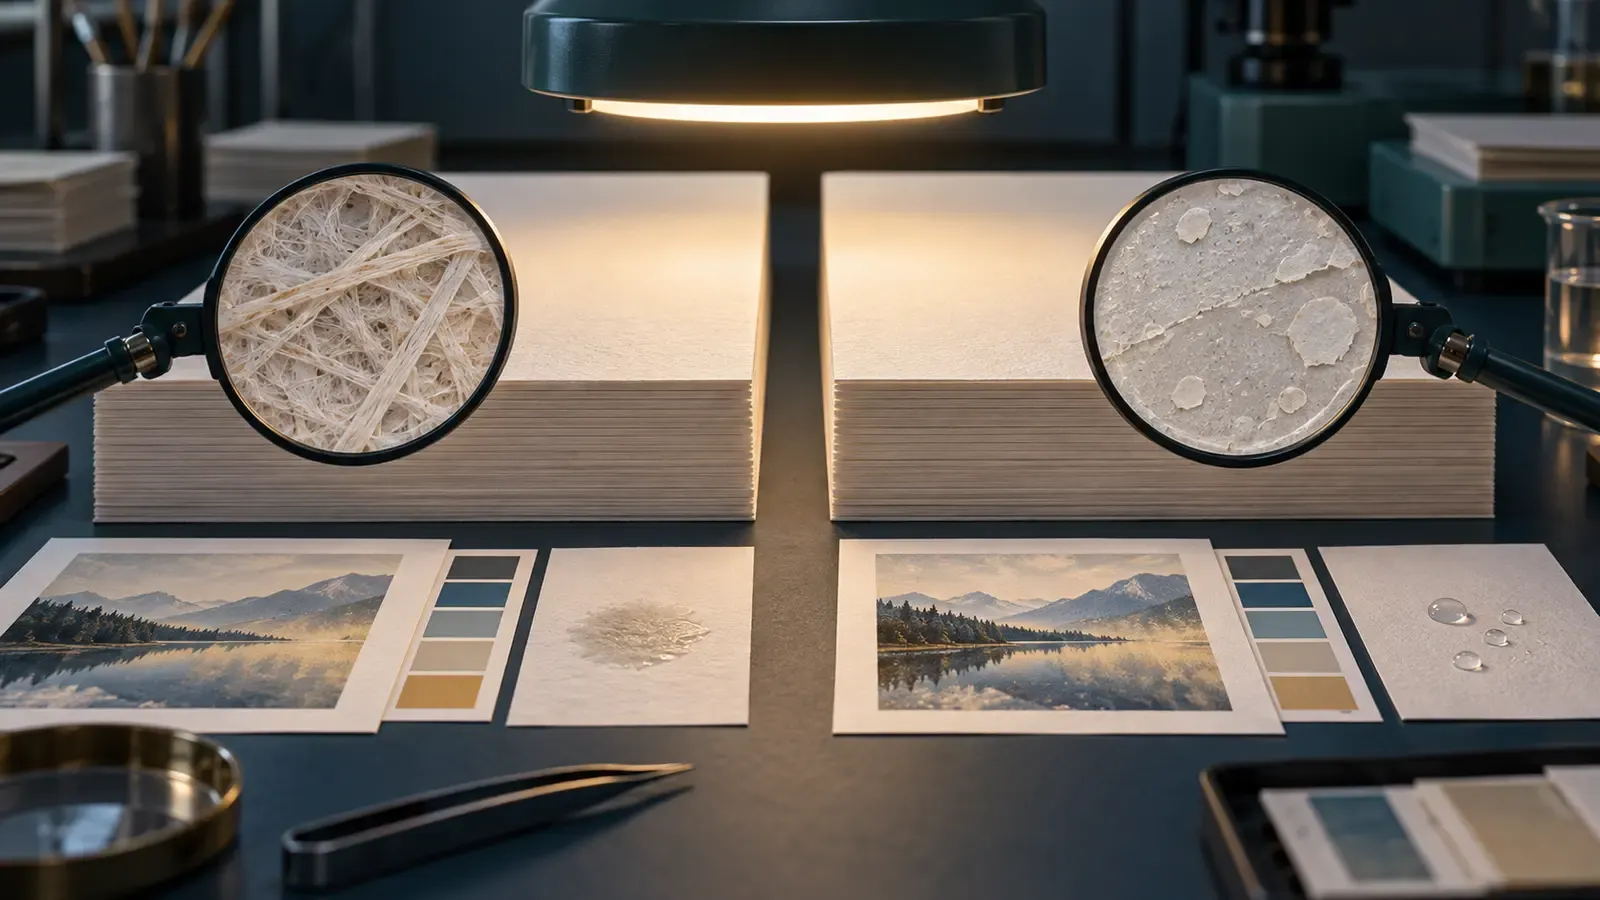
Two paper or board lots can satisfy the same commercial specification yet behave differently because of coating, fibre, moisture, storage, transport or manufacturing variation. Lot traceability connects receiving and inspection evidence to job consumption and quality results, allowing the factory to contain risk, explain variation and improve future purchasing.
The matching label
The delivery label names the correct grade, weight and supplier. Purchasing sees no discrepancy. Warehouse issued the material against the job exactly as requested.
On press, colour takes longer to stabilise. At die-cutting, the crease behaves differently. The previous order ran cleanly under what everyone calls “the same paper.”
The description is the same. The physical history is not.
Give every received lot an identity
Capture supplier, supplier lot, internal lot, receipt, quantity, unit, certificate or specification, inspection state and storage location. Preserve the link when rolls or pallets are split.
An internal lot helps the factory manage material consistently even when supplier documentation varies. It should never erase the supplier reference needed for a claim or investigation.
Labels must survive normal handling and make the next decision obvious: what is this, how much remains, is it released, and where may it be used?
Inspect according to risk
Not every receipt needs the same test. Define checks by material, supplier history, customer requirement and process sensitivity.
Possible evidence includes dimensions, weight, moisture, coating, shade, surface condition, certificate review and packaging damage. Sample size and acceptance rules should be explicit.
Record the result against the lot, not only a paper form. If the material is conditionally released, state the restriction and owner. A “received” status should not imply it is production-ready.
Preserve storage and conditioning history
Paper and board respond to environment. Time, humidity, temperature and wrapping condition can affect production even when the supplier lot is sound.
Record unusual storage, exposure, damage and conditioning where relevant. Use first-in-first-out rules carefully when customer or process requirements demand a specific lot.
If material moves between warehouses or plants, maintain the lot identity and quantity. Transfer should not create a fresh anonymous stock balance.
Link issue and return to the job
When material is issued, record the job, batch, quantity and lot. If more than one lot feeds the run, preserve each contribution.
Unused material returning to stock should retain lot and condition. Identify opened rolls, partial pallets and usable remnants according to practical rules. Do not merge physical material merely because the item code matches.
The traceability pillar shows how this material relationship supports forward and backward investigation.
Compare lot behaviour with evidence
Connect material lots to setup time, speed, spoilage, print quality, cutting, folding, gluing and customer complaints. Patterns across jobs can reveal variation invisible at receiving.
Do not conclude too quickly that the lot caused every difference. Compare artwork, machine, settings, environment and operator evidence. The lot relationship defines the population to investigate; it does not replace root-cause analysis.
When a repeat pattern appears, purchasing can discuss a precise body of evidence with the supplier.
Contain a suspect lot proportionately
If a lot is suspected, identify remaining stock, WIP, finished goods and shipments that consumed it. Hold only the credible affected population while evidence is gathered.
Record the containment decision, quantities and locations. If some output is released after additional inspection, preserve that evidence. If mixed lots were used, acknowledge the wider scope.
Fast containment protects customers and prevents unnecessary disposal of unrelated stock.
Manage substitutions openly
Material shortages may require an alternative grade or lot. Confirm technical suitability, customer approval, cost, imposition, yield and process settings before release.
Record which output used the substitute. Do not overwrite the original bill of material until history can no longer explain the actual job.
The substitution may save delivery while changing margin or future repeatability. Both outcomes belong in the job record.
Give purchasing usable supplier feedback
Supplier evaluation should combine on-time delivery with lot acceptance, variation, claim response, yield effect and total operational cost.
A cheap material that causes longer setup, lower speed or repeated spoilage may not be the lowest-cost choice. Conversely, one abnormal lot should not condemn a reliable supplier without investigation.
Use comparable jobs and clear evidence. This creates a commercial conversation grounded in production reality.
Measure material genealogy quality
Monitor lots with missing supplier reference, production issues without lot identity, returned material merged into unknown stock, mixed-lot runs without allocation and complaints that cannot be traced to material.
Also measure time to identify affected jobs and shipments from a selected lot. Retrieval speed reveals whether records are truly connected.
Start with one sensitive substrate
Choose a board, paper or film that frequently affects yield or quality. Map receiving, storage, issue, production and return. Run forward and backward tests on completed jobs.
Fix the points where identity breaks. Then add practical scanning or automatic capture. Expand to other materials according to risk and value.
This focused approach produces operational learning faster than attempting perfect traceability across every consumable at once.
Frequently asked questions
Build a material exception workflow
When receiving or production detects unusual material, create one exception linked to the lot. Record observed condition, evidence, quantity, location, immediate containment and decision deadline.
Possible dispositions include release, conditional use, additional test, supplier return, downgrade, rework or scrap. Show which jobs are waiting and the latest decision time before their schedule changes.
If a supplier concession or replacement is agreed, keep it with the same event. Purchasing, quality, warehouse and planning then act from one decision rather than separate email threads.
Compare samples without losing context
Retained samples are valuable only when identity and storage preserve their meaning. Label supplier lot, internal lot, receipt and inspection condition. For production samples, include job, batch, artwork version, machine and time.
Define how samples are stored and how long they remain representative. Light, moisture and handling can change paper and colour. An unlabelled sheet found beside the press is not a reliable standard.
When comparing a complaint or new lot, use a consistent viewing or test method. Record the conclusion and person authorised to accept variation.
Improve inventory decisions
Lot visibility can support more than investigation. Planners can choose stock by customer approval, age, condition and job need. Warehouse can avoid creating unusable remnants. Purchasing can see whether a large balance belongs to a restricted lot.
Use shelf-life or conditioning rules where relevant, but avoid automatic first-in-first-out when it conflicts with batch consistency or customer requirement. The picking rule should state why a particular lot is preferred.
When stock is reallocated, preserve the demand that lost protection. Material efficiency should not create a hidden production shortage.
Close the supplier learning loop
At regular reviews, show evidence by lot: acceptance, yield, setup, speed, defect, claim and response. Compare equivalent materials and jobs fairly.
Ask what both parties can change. Packaging at delivery, certificate format, lot size, conditioning advice or notice of process change may improve stability without changing the headline specification.
Confirm actions on future receipts and production results. A claim credit resolves one transaction; shared learning reduces the next disruption.
Is the supplier lot number enough?
It is essential but may not reflect internal splits, condition or location. Preserve it while using an internal identity suited to factory control.
Can two lots be mixed in one production run?
Where specification allows, yes. Record both lots and affected output because the possible investigation scope becomes wider.
Should all returned material go back to available stock?
Only after quantity, lot, condition and release state are confirmed. Open or damaged material may need restriction or inspection.
How does lot traceability improve sustainability?
It supports better yield analysis, proportionate containment and credible recovery decisions, reducing the need to discard unrelated material.
The specification needs a history
Create a lot review for materials inside the near-term schedule. Surface conditional stock, expiring decisions, mixed-lot risk, inspection delay and jobs without protected released quantity. Review only exceptions requiring action.
When production reports unusual behaviour, record the lot before material is moved or remnants are merged. Preserve a sample where investigation value justifies it. Fast identification is often more important than a long initial description.
Close the loop after the job: did the suspected lot actually correlate with setup, yield or quality? Was the supplier evidence complete? Should inspection, storage or planning change?
This routine makes lot traceability a production aid rather than paperwork reserved for claims. It also improves the fairness of supplier conversations because conclusions are tested against comparable evidence.
Material descriptions make purchasing possible. Lot identity makes production evidence possible.
When the paper behaves differently, the factory can move beyond memory and generalisation. It can identify the physical lot, the jobs it touched, the results it produced and the action that protects both customer and next order.