

The Waiting Factory: Where Apparel Lead Time Goes When Nobody Is Sewing
Garment lead time rarely disappears at the needle. It accumulates while orders wait for decisions, approvals, material, capacity and permission to move.
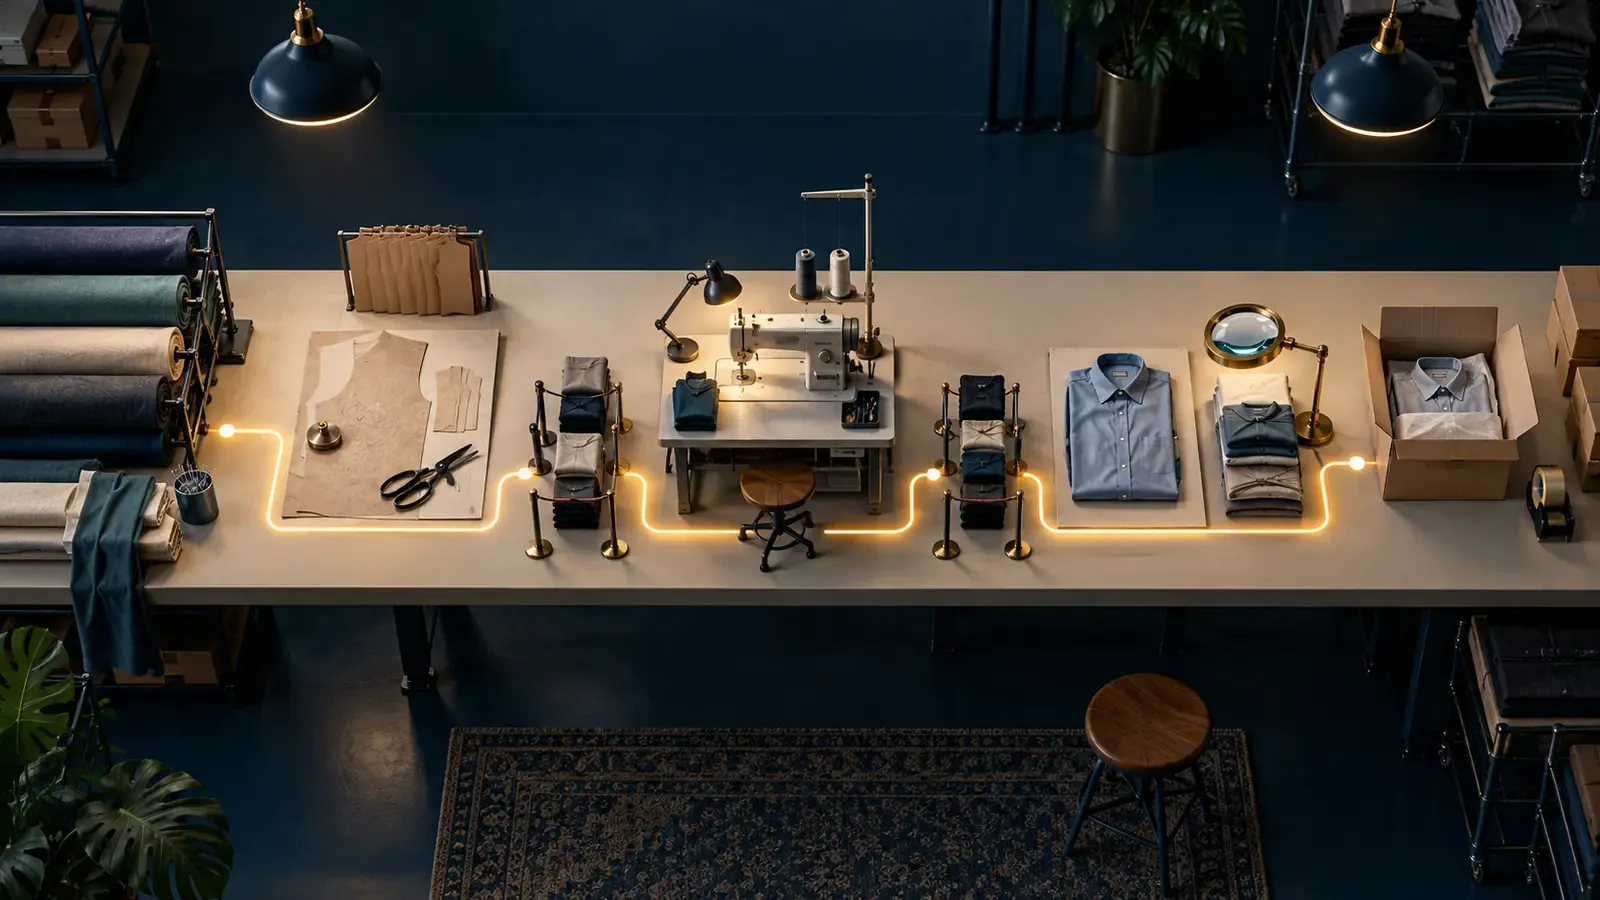
At 2:10 on Wednesday afternoon, a garment order has already spent 37 days inside the business. Yet only a fraction of that time has involved cutting, sewing, finishing or packing. For most of its life, the order has been stationary.
It waited for a buyer comment, then for a revised sample. It waited for material confirmation, laboratory approval, allocation, a free line, a machine attachment and a final decision about shipment. Every pause had an explanation. Together, the explanations became the lead time.
Managers often search for speed at the needle because production is visible. The larger opportunity may be the quiet time between productive events.
The short answer
Garment manufacturing lead-time reduction begins by separating touch time from waiting time. Manufacturers need one timeline for the order, visible entry and exit conditions for each stage, named owners for blocked decisions, limits on work-in-progress and reliable events connecting sample, material, production, quality and shipment.
The objective is not to make people rush. It is to stop the order waiting invisibly for permission, evidence or capacity that nobody is managing as time.
The calendar and the garment tell different stories
A production calendar shows planned milestones: order confirmation, sample approval, material arrival, cutting, sewing and shipment. It rarely shows the days consumed before a milestone can begin or after the work is technically complete but not released.
The garment experiences a different timeline. It waits in an inbox, on a rack, inside a warehouse status, between operations and beside an inspection table. Some waiting protects quality or enables an economic batch. Some is caused by uncertainty, queues and unclear ownership.
Lead-time improvement requires distinguishing necessary protection from unmanaged delay. Removing every buffer would make the system fragile. Leaving every wait unexplained makes it slow.
Seven places time hides
1. Approval queues
The decision may take five minutes, but assembling evidence, finding authority and chasing a reply consumes days. The Five-Minute Approval That Makes a Garment Order Wait Five Days shows how to manage approval as a timed operational dependency.
2. Work-in-progress
Bundles between operations look like production, but their age and imbalance may be writing tomorrow's shortfall. That Pile Between Sewing Operations Is Already Writing Tomorrow's Schedule treats WIP as a flow signal rather than harmless inventory.
3. Late quality discovery
Final inspection can detect a problem after thousands of pieces share the same method. Final Inspection Is the Most Expensive Time to Discover a Process Problem moves learning to first output and in-line control.
4. External production blind spots
Subcontracting may add capacity but remove direct visibility. The Invisible Factory Outside Your Factory asks how order identity, progress, quality and due-diligence evidence travel beyond the main site.
5. Machine readiness
Equipment can exist without being configured, maintained or supported for the incoming style. The Machine Was Available Until the Style Arrived connects maintenance and setup to the production promise.
6. Changeovers
Ten minutes multiplied across forty operators becomes a substantial loss, especially when first-quality output takes longer to stabilise. The Hidden Cost of a Garment Changeover examines the coordinated restart behind a new style.
7. Hidden buffers
Every department adds protection to its own promise, but the order can still run late because nobody manages the combined buffer. Every Team Adds Two Days. Why Is the Garment Order Still Late? replaces private padding with visible protection and priorities.
The final question is whether the organisation learns. The Month-End Review That Should Change How the Factory Runs Next Month turns recurring waits into changes to standards, workflows and assumptions.
Touch time is only the visible island
Touch time is the period during which useful transformation or verification occurs: a pattern is amended, fabric is inspected, panels are cut, a seam is sewn, a garment is checked. Waiting time sits around those activities.
The distinction is not always absolute. Material may rest for conditioning; that time can be technically necessary. A batch may wait to make testing economic. The important question is whether the reason, duration and release condition are known.
Map a small number of real orders from confirmation to shipment. For each stage, record when the order arrived, when work began, when work ended and when the next stage accepted it. The gaps often tell a more useful story than the activity durations.
Every queue has a rule, even when nobody wrote it
Orders do not wait randomly. They are sequenced by explicit priorities or informal habits: largest customer first, loudest escalation first, complete batches first, oldest request first, easiest decision first. If the rule is invisible, teams experience the queue as politics.
Make priority logic visible. A queue may consider delivery consequence, decision window, material expiry, line stability, customer agreement and recovery cost. The rule does not need to remove judgement. It should make exceptions to the rule explainable.
An honest queue is more useful than multiple teams believing their order is next.
The cost of waiting compounds
A day lost early may appear harmless because the shipment date is distant. Yet early waiting consumes options. A delayed approval compresses material ordering; compressed material timing reduces shipping choices; late material destabilises the line; unstable production pushes quality and logistics toward expensive recovery.
This is why elapsed days alone are insufficient. Record which options disappeared during the wait. The economic cost may include higher purchasing, overtime, smaller batches, premium freight, missed consolidation, extra handling and management attention.
The exception economy explains how decision windows close. The waiting factory is the time dimension of the same operating reality: when nothing moves, risk can still grow.
Give each stage an entry and exit condition
Milestones such as “sample complete” or “fabric arrived” are too broad. Define what allows the next decision.
An approval stage enters when the correct evidence and effective version are available. It exits when the authorised decision is recorded and downstream records update. Material readiness enters with identified receipts and exits when the relevant quantity is inspected, allocated and available for the required cut date. Line readiness exits when people, machines, method, material and first-quality controls are prepared.
Clear conditions reveal partial completion. They also prevent work being passed downstream with a hidden dependency.
Flow is an agreement between functions
One department cannot optimise total lead time alone. Purchasing can order earlier and create excess. Production can build WIP and appear busy. Quality can protect standards through extra inspection while queues grow. Logistics can preserve low freight cost by waiting for consolidation.
The order needs a cross-functional flow owner or operating rhythm that sees the combined promise. Trade-offs should be explicit: which waiting protects value, which only protects a departmental metric, and which threatens a future decision.
What connected garment operations contribute
ACC describes Venus as an ERP platform for apparel and garment manufacturing, connecting sample, order, material, costing, production and multi-factory processes. See the official Venus overview for current product scope.
The value for lead time is a shared event history. Instead of reconstructing dates from messages, the organisation can connect effective approvals, material status, production events, quality holds and shipment decisions to the same order identities.
Execution data can show where work is and when it last moved. ERP context explains why that movement matters commercially. Neither replaces management; together they make waiting visible enough to manage.
A 30-day waiting-time study
Choose six orders: a repeat style, a new construction, a changed order, a difficult material, an external process and a rush programme. Do not select only failures.
For each order, create one elapsed-time map. Mark productive activity, technically required waiting, queue waiting, decision waiting and rework. Record the owner and release condition for every gap longer than an agreed threshold.
At the end of the month, rank waits by total time, frequency, option loss and recovery cost. Fix one recurring interface—not ten isolated symptoms. Examples include incomplete approval packets, missing machine-readiness checks or unclear material-release rules.
Measures that keep speed honest
Lead time can improve on paper if teams move dates, release work prematurely or build more inventory. Use a balanced view:
- total elapsed lead time by order type;
- touch-time-to-waiting-time relationship;
- approval and decision latency;
- WIP age and time between operations;
- time to first acceptable output;
- queue age before external processing;
- recovery cost used to protect delivery;
- on-time performance against original and current commitments.
Read quality, cash and margin beside speed. Faster is valuable when it produces a more reliable promise, not merely an earlier internal status.
Frequently asked questions
What is garment manufacturing lead time?
It is the elapsed time required for an order or product to move through relevant commercial, development, material, production, quality and delivery stages under a defined start and end point.
Why is waiting time often larger than sewing time?
Orders spend time in approval, material, capacity and WIP queues. The productive operations may be short relative to the delays before work can begin or move onward.
Is all waiting waste?
No. Some waiting protects quality, conditioning, batch economics or risk. It should still have a known purpose, duration and release condition.
Where should a factory start reducing lead time?
Map a few live orders end to end and identify recurring gaps that close valuable options. Begin with one cross-functional handoff rather than asking every department to work faster.
Can ERP reduce lead time by itself?
ERP can connect identities, events and ownership, but operating rules and decisions must also change. Technology makes the wait visible; management redesigns it.
The fastest factory is not the busiest
A busy floor can contain large queues. A quiet decision can release more lead time than another hour of sewing. The competitive question is not how much activity the organisation can display, but how smoothly an order can move from one valid state to the next.
When the business sees waiting as part of production, it begins asking better questions. Why is the order here? What evidence or decision releases it? Who owns that decision? Which option disappears if it waits until tomorrow?
The needle matters. So does every hour before the needle is allowed to move.
Run a one-order waiting audit
Management does not need a transformation programme to expose the first layer of delay. Choose one recently completed order that people remember well and reconstruct its elapsed journey. Use timestamps, handover records and physical evidence where available. Do not begin by asking who caused the delay; begin by asking what the order was waiting for.
Create a simple sequence from commercial confirmation to dispatch. For every major interval, classify the time as productive work, necessary process time, planned protection or avoidable waiting. If the classification is disputed, record the uncertainty. The argument itself often reveals that different teams hold different versions of the order history.
Then examine five moments:
1. the longest wait;
2. the oldest unconfirmed assumption;
3. the first signal that the plan was weakening;
4. the first management response;
5. the recovery action that consumed the most resource.
This audit creates a shared picture without pretending that one order represents the whole factory. Repeat it across several order types and patterns begin to emerge.
Design daily management around ageing work
Most daily boards emphasize what is due today. Add what has waited too long. An approval outstanding for thirty-six hours, a bundle stationary beyond the normal interval or an external process without fresh evidence may deserve attention before its formal due date.
Ageing is useful because it exposes risk while choices still exist. The team can clarify a decision, rebalance flow, contain quality, prepare an alternative resource or escalate a missing confirmation. After the due date passes, those same actions become recovery.
A concise daily waiting review can ask:
- What work has not moved since the last review?
- What evidence are we waiting for?
- Who has authority to release the next step?
- What is the latest safe action time?
- Which wait is blocking several downstream tasks?
Keep the discussion linked to named orders and milestones. A long list of “pending” items without age, consequence or ownership simply gives uncertainty a new screen.
Avoid improving one queue by moving it elsewhere
Local efficiency projects can relocate waiting. Cutting may release larger batches to stay busy, creating a sewing queue. Sewing may push incomplete quantities into finishing to protect its output. Merchandising may request every approval as urgent, overwhelming the decision maker and lengthening all responses.
Evaluate improvement through end-to-end elapsed time and commitment performance. If one department’s utilization rises while WIP, rework or downstream waiting increases, the order has not improved.
This is why the pillar view matters. The individual articles in this series examine specific rooms—the inbox, the WIP rack, the inspection table, the subcontractor, the machine setup and the review meeting—but management must reconnect them into one buyer-order journey.
A practical ninety-day sequence
In the first thirty days, define shared milestone language and measure a few completed orders. In the next thirty, introduce ageing triggers at the two or three largest recurring waits. In the final thirty, test operating changes and compare their effect on elapsed time, quality and recovery effort.
Do not wait for perfect data. Start with evidence strong enough to support a decision, then improve the record where uncertainty repeatedly blocks action. The objective is a factory that learns to see waiting early—and develops the confidence to remove it without destabilizing the work around it.